
Mate Precision Technologies · USA
Mate tooling for sheet metal punch presses
Mate Precision Technologies makes punches and dies for CNC turret punch presses, compatible with Amada, Trumpf, Euromac, LVD Strippit, Prima Power / Finn-Power, Salvagnini, and Murata Wiedemann. Lang & Sin is the exclusive representative for Mate in Romania. The Technical Center has a die clearance guide and a tool maintenance guide.
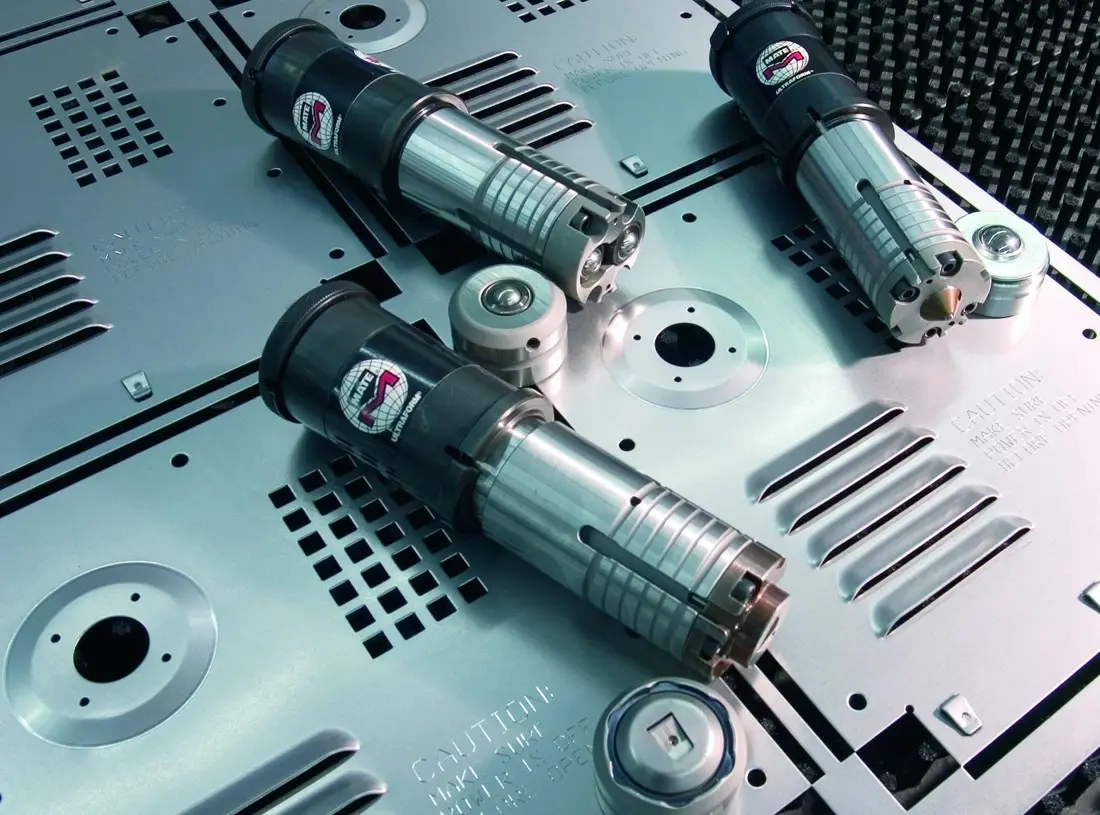
About Mate Precision Technologies
Mate Precision Technologies is an American manufacturer of industrial tooling, founded in 1962 in Minneapolis, Minnesota, as Mate Punch and Die Co. The company started out specializing in punch press tooling, and over more than six decades has expanded its range to press brake tooling, multi-tool systems, and, since 2021, zero-point workholding.
In 2009, Mate received the Manufacturer of the Year award from the Manufacturers' Alliance. Over the years, the company has also developed dedicated tooling systems for other major machine builders, including Nova® for Prima Power punch presses and Marathon® for Murata Wiedemann machines.
In 2026, Mate became part of the Trumpf family through a strategic partnership.
Punching tools for Amada machines
For Amada thick turret punch presses, Mate offers the Ultra® system (UltraTEC®, Ultra XT™, Original Style) on stations A (½"), B (1¼"), C (2"), D (3½") and E (4½"), and the AMX™ system for machines with ABS clamping. Multi Tools, forming tools and special applications fit the same stations.
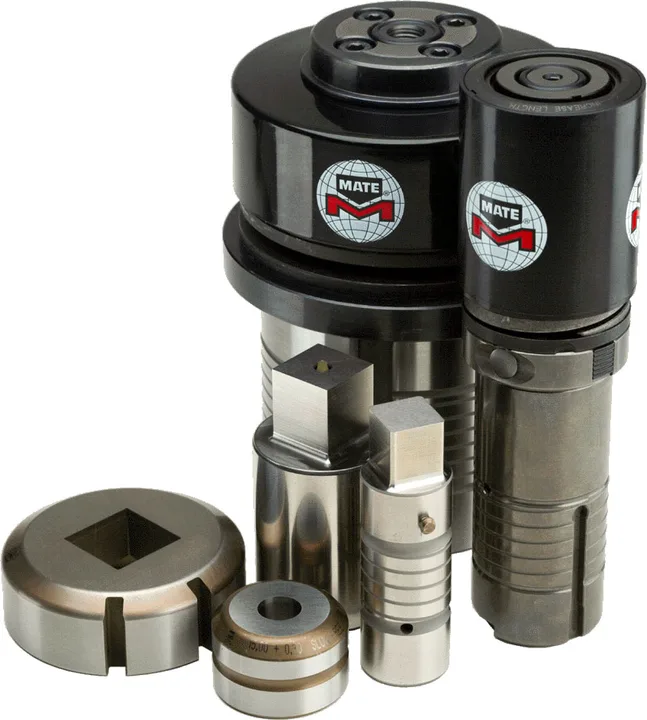
UltraTEC®
Materials and hardening · tool-free "click" length adjustment · Heavy Duty, Fully Guided, and Ultra Light variants
Also fits: Euromac, Prima Power / Finn-Power
UltraTEC®
Materials and hardening · tool-free "click" length adjustment · Heavy Duty, Fully Guided, and Ultra Light variants
Also fits: Euromac, Prima Power / Finn-Power
The flagship of the Thick Turret line: Mate's own comparison chart rates it highest on overall value, cost, and regrind life.
- Available stations
- A (1/2")
- B (1-1/4")
- C (2")
- D (3-1/2")
- E (4-1/2")
- Punch materials
- premium high-speed steel (HSS)
- M4PM™ optional, A and B stations: particle metallurgy, with 100% more wear resistance and 50% more toughness than conventional tool steel, and twice the interval between regrinds in customer trials, per Mate
- Max. material thickness recommended by Mate (standard system)
- aluminum 3.99 mm
- mild steel 3.99 mm
- stainless 2.90 mm (stations A–D)
- Extra regrind life vs. Original Style
- 0.118"(3.00mm) on A/B stations
- 0.212"(5.38mm) on C/D/E stations
- Usable regrind life, comparative example
- station B, 1.50 mm material, 3.00 mm die penetration: 0.408"(10.36mm) with Ultra® stripper, vs. 0.170"(4.32mm) with Original Style stripper
- stations C/D/E, same conditions: 0.512"(13.00mm) with Ultra® stripper
- "Click" length adjustment
- 0.006"(0.15mm)/click on station A
- 0.008"(0.20mm)/click on stations B/C/D/E
- no shims or separate tools
- Back taper
- 1/4° + near-polished flanks: reduces friction and galling
- Lubrication
- internal and external spiral grooves
- Guides
- hardened, ground: reduce turret bore wear
- Maxima™ coating
- available as an option: zirconium titanium nitride (ZrTiN), recommended for 3000- and 5000-series aluminum, galvanized sheet, stainless steel, and materials where lubricant can't be used; Mate cites real field tests with 2 to 10 times longer tool life
- SLUG FREE® die regrind life
- up to 0.125"(3.20mm)
- SLUG FREE® dies: standard: eliminates slug pulling, reduces tool breakage, improves hole quality
- Interchangeable with existing OEM inventory
Compatibility and dimensions
Max. punch diameter/diagonal by station (same base geometry for standard Ultra TEC®, Ultra XT™, and Original Style punches).
| Station | Max. punch diameter/diagonal | Max. die size (incl. clearance) |
|---|---|---|
| A (1/2") | 0.500"(12.70mm) | 0.559"(14.19mm) |
| B (1-1/4") | 1.250"(31.75mm) | 1.309"(33.24mm) |
| C (2") | 2.000"(50.80mm) | 2.054"(52.17mm) |
| D (3-1/2") | 3.500"(88.90mm) | 3.554"(90.27mm) |
| E (4-1/2") | 4.500"(114.30mm) | not specified |
A (1/2")
- Max. punch diameter/diagonal
- 0.500"(12.70mm)
- Max. die size (incl. clearance)
- 0.559"(14.19mm)
B (1-1/4")
- Max. punch diameter/diagonal
- 1.250"(31.75mm)
- Max. die size (incl. clearance)
- 1.309"(33.24mm)
C (2")
- Max. punch diameter/diagonal
- 2.000"(50.80mm)
- Max. die size (incl. clearance)
- 2.054"(52.17mm)
D (3-1/2")
- Max. punch diameter/diagonal
- 3.500"(88.90mm)
- Max. die size (incl. clearance)
- 3.554"(90.27mm)
E (4-1/2")
- Max. punch diameter/diagonal
- 4.500"(114.30mm)
- Max. die size (incl. clearance)
- not specified
Variants
Ultra TEC® Heavy Duty
For thicker material or noise reduction: recommended from 0.118"(3.00mm) material thickness up. Thicker-wall construction (1° back taper per side, vs. 1/4° standard), heavy-duty springs on the B station, rooftop shear available on B/C/D stations. Minimum tool size: 0.250"(6.35mm). Max. thickness recommended in the Heavy Duty variant: aluminum 6.35 mm on A/B stations and 8.00 mm on C/D, mild steel 4.57 mm on station A and 6.35 mm on B/C/D, stainless 3.99 mm on station A and 4.57 mm on B/C/D.
Ultra TEC® Fully Guided
The punch is held rigid at two extreme points (tip and back) to prevent lateral movement. Stripper clearance to the punch is 0.03 mm (vs. 0.06 mm standard): tighter guiding for hole accuracy and longer tool life. Available on B/C/D stations, with 0.008"(0.20mm) "click" adjustment.
- Slitting / Clamp Clearing variant (D, E stations): strippers allow punching as close as 15 mm from an upward-formed edge, dies as close as 20 mm from a downward-formed edge, without repositioning work-holder clamps.
Ultra Light™
Reduced-force canisters for thin, decorative, or reflective material: reduces sheet marking and noise (Mate states up to 10 dB reduction). A-station canisters apply 70% of standard Ultra TEC stripping force, B-station canisters 60%. Available on A/B/C/D/E stations.
Ultra TEC® punches are fully interchangeable with existing OEM tooling inventories (Wilson HP™/HP2™/WLS®, Amada Standard, Amada ABS, Amada Z-Standard/Z-ABS, Amada NEX, Wilson Nisshinbo Multi Tool, and others), per Mate's own compatibility matrix.
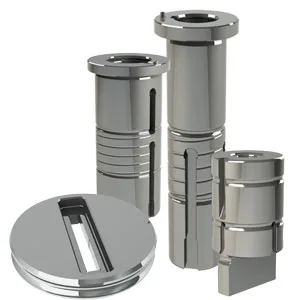
AMX™
100% compatible with Amada ABS assemblies · A–E stations · Maxima™ and Nitride coatings available
AMX™
100% compatible with Amada ABS assemblies · A–E stations · Maxima™ and Nitride coatings available
Full conversion to Amada® ABS compatibility, with fit into Mate Ultra TEC® tool holders as well.
- Compatibility
- 100% with Amada® ABS assemblies and tool holders
- AMX tool holders also fit Mate Ultra TEC® and Ultra TEC® Fully Guided systems
- Available stations
- A, B: punches and stripper guides
- C, D, E: punches and strippers
- D, E: dedicated slitting system
- Materials
- M2 high-speed steel, OEM-equivalent
- Lubrication channels
- precision gun-drilled on A/B-station punches, replicating the internal Amada lubrication path
- Back taper
- 1/4°: reduces galling
- Orientation pin
- hardened: accurate piece-part positioning
- Extra regrind life
- 0.118"(3.00mm) on A/B-station stripper guides
- 0.078"(2.00mm) on C/D/E stations
- Available coatings
- Maxima™
- Nitride
- SuperMax™ (no technical detail published by Mate)
The AMX Seal Kit (A/B stations) converts an existing Mate Original Style punch assembly to ABS compatibility, without buying a new punch. RapidSet™ adjustable canisters are also available for Original Style and AMX tooling on A/B stations: single-screw length adjustment without removing the canister from the guide, with roughly 67% more usable regrind life than standard Mate Original Style canisters.
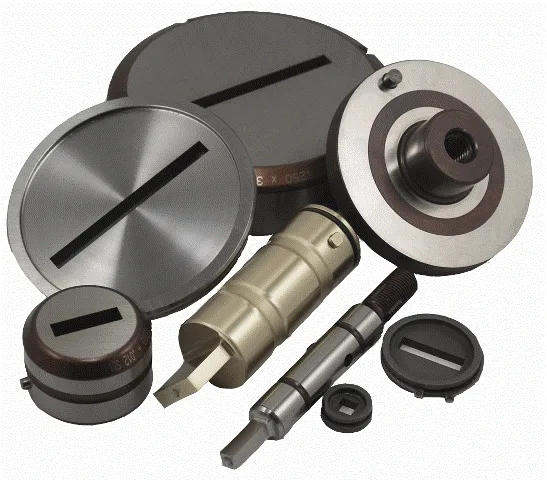
MXC™
100% compatible with Wilson HP™/HP™ WLS®/HP™ ABS · DuraSteel™ steel · full dimension table
Also fits: Euromac, Prima Power / Finn-Power
MXC™
100% compatible with Wilson HP™/HP™ WLS®/HP™ ABS · DuraSteel™ steel · full dimension table
Also fits: Euromac, Prima Power / Finn-Power
"The superior alternative" for Wilson HP™ tooling users: 100% compatible, with the option to fit Ultra TEC®/Ultra XT™ guides as well.
- Compatibility
- 100% with Wilson HP™, HP™ WLS®, HP™ ABS (formerly Series 90®)
- fits Ultra TEC®/Ultra XT™ guides with an adapter or pin swap
- Materials
- DuraSteel™: high-speed steel with increased vanadium and tungsten content, 100% longer between regrinds than conventional tool steel
- Maxima™ coating
- available as an option: zirconium titanium nitride (ZrTiN), recommended for 3000- and 5000-series aluminum, galvanized sheet, stainless steel, and materials where lubricant can't be used; Mate cites real field tests with 2 to 10 times longer tool life
- Punch orientation
- hardened double-D key
- SLUG FREE® dies: standard: eliminates slug pulling, reduces tool breakage, improves hole quality
Compatibility and dimensions
Critical dimensions, verbatim from Mate's technical data sheet (mxc-tooling-system.pdf).
| Station | Max. punch diagonal | Overall length | SBR |
|---|---|---|---|
| A | 0.500"(12.70mm) | 4.640"(117.86mm) | 0.740"(18.80mm) |
| B | 1.250"(31.75mm) | 3.957"(100.51mm) | 0.740"(18.80mm) |
| C | 2.000"(50.80mm) | 2.360"(59.94mm) | 1.004"(25.50mm) |
| D | 3.500"(88.90mm) | 2.360"(59.94mm) | 1.004"(25.50mm) |
| E | 4.500"(114.30mm) | 2.360"(59.94mm) | 1.004"(25.50mm) |
A
- Max. punch diagonal
- 0.500"(12.70mm)
- Overall length
- 4.640"(117.86mm)
- SBR
- 0.740"(18.80mm)
B
- Max. punch diagonal
- 1.250"(31.75mm)
- Overall length
- 3.957"(100.51mm)
- SBR
- 0.740"(18.80mm)
C
- Max. punch diagonal
- 2.000"(50.80mm)
- Overall length
- 2.360"(59.94mm)
- SBR
- 1.004"(25.50mm)
D
- Max. punch diagonal
- 3.500"(88.90mm)
- Overall length
- 2.360"(59.94mm)
- SBR
- 1.004"(25.50mm)
E
- Max. punch diagonal
- 4.500"(114.30mm)
- Overall length
- 2.360"(59.94mm)
- SBR
- 1.004"(25.50mm)
Market note: on A/B stations, MXC punch availability may be restricted in certain countries for patent licensing reasons (per a list Mate publishes, covering several EU and North American markets). Romania does not appear on that list, but we recommend confirming directly with Mate before ordering.
Keep in mind: Fitting MXC C/D/E punches into Ultra TEC®/Ultra ABS® guides requires a dedicated HP™ adapter; shaped MXC ABS Style B-station punches cannot be adapted to Ultra XT™ guides: Ultra TEC only.
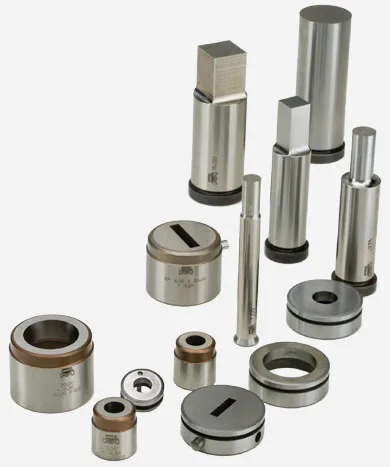
MT™ Tooling System
Three sizes: 8, 16, and 24 mm · SLUG FREE® dies standard · Maxima® coating optional
Also fits: Prima Power / Finn-Power
MT™ Tooling System
Three sizes: 8, 16, and 24 mm · SLUG FREE® dies standard · Maxima® coating optional
Also fits: Prima Power / Finn-Power
Mate's general-purpose Multi Tool line, compatible with Mate-manufactured multi-tool assemblies.
- Available sizes
- 8 mm
- 16 mm
- 24 mm (max. punch diameter/diagonal)
- Max. material thickness recommended by Mate
- MT 8 mm: aluminum 3.99 mm, mild steel 3.00 mm, stainless 1.98 mm
- MT 24 mm: aluminum 5.00 mm, mild steel 5.00 mm, stainless 2.49 mm
- Materials
- high-speed steel (HSS) punches, resistant to edge wear
- Back taper
- 1/4° + near-polished flanks: eliminates galling
- Punch-to-stripper clearance
- tight: superior guiding
- SLUG FREE® dies: standard: eliminates slug pulling, improves hole quality
- Maxima® coating: available as an option, for extended tool life
Dedicated service tool sets (stripper/die puller, magnet pen, retrieving tool) are available for each size, plus a complete kit covering all three.
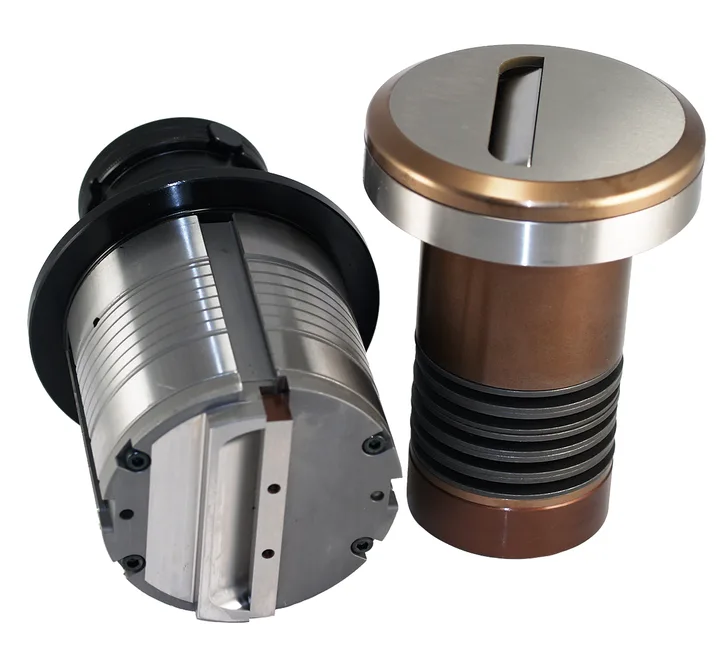
Ultraform®
Three tiers: push-button adjustment, manual adjustment, fixed length · inserts interchangeable across all three · B–E stations
Also fits: Euromac, Prima Power / Finn-Power
Ultraform®
Three tiers: push-button adjustment, manual adjustment, fixed length · inserts interchangeable across all three · B–E stations
Also fits: Euromac, Prima Power / Finn-Power
An adjustable-length tool holder with interchangeable inserts: buy one holder, swap only the insert for each form.
- Available stations
- B (1-1/4")
- C (2")
- D (3-1/2")
- E (4-1/2")
- Adjustment below the shoulder
- maintains the ram-to-tool gap at top of stroke: eliminates the risk of the ram striking the tool and damaging the turret
- Standard angle settings
- 0°
- 90°
- 180°
- 270°
- Guides
- hardened, with lubrication grooves
- Insert interchangeability: every insert works in any of the three holders: Ultraform®, Ultraform XT™, Ultraform FX™
Variants
Ultraform® (top tier)
Push-button length adjustment, no disassembly, in 0.05 mm increments: the finest adjustment of the three. Internal and external lubrication channels, compatible with most punch press lubrication systems.
Ultraform XT™ (mid tier)
Manual adjustment: loosen the screws, turn the punch head to the desired length. External lubrication grooves only; compatibility with the machine's lubrication system is optional, not built in.
Ultraform FX™ (fixed length)
For machines with precision stroke control at the machine level: eliminates the need for tool-side length adjustment. Not a weaker option, but the right tool for machines with their own stroke control.
The Ultraform® holder works as a platform for several Mate tools, not just forming inserts: the same B-station holders accept the Rollerball Deburr™ insert (deburring at the press), the Sheetmarker™ marking tool, and the Rollerball™ insert, which in an Ultraform® holder gains fine form-depth adjustment even on machines without precise stroke control. One holder already on hand covers several operations this way.
Keep in mind: Original Style forming tools (B station only, no interchangeable inserts) are dedicated to a single material-thickness-machine combination: moving them to another machine can damage the tool or the press. For any application where the tool will be reused across configurations, the Ultraform® family is the right choice.
Roller Solutions™
Four variants: ribbing, shearing, angled cutting, offsetting · strict compatibility with servo/auto-index machines
Also fits: Euromac, Prima Power / Finn-Power
Roller Solutions™
Four variants: ribbing, shearing, angled cutting, offsetting · strict compatibility with servo/auto-index machines
Also fits: Euromac, Prima Power / Finn-Power
An alternative to progressive (multi-hit) forming: runs at table travel speed, no separate secondary operations.
- Operating principle
- runs at speed equal to programmed table travel: does not slow the machine down, unlike progressive forming
- works through auto-indexing, can follow any contour
- features can start or end anywhere on the sheet
- Available station
- B (1-1/4") only
Compatibility and dimensions
Machine compatibility: a strict technical requirement (servo/auto-index motion control), not just a mechanical fit.
| Brand | Compatibility condition |
|---|---|
| Amada | servo-electric ram machines (EM, AE, AC, ACIES, etc.); Vipros with 18p controller; Apelio with 160iL controller |
| Euromac | MTX auto-index machines shipped after March 3, 2005; ZX auto-index machines shipped after February 18, 2005 |
| Prima Power | machine serial number ≥ 7.8, or serial number 7.7 with PLC software ≥ 75.11 |
Amada
- Compatibility condition
- servo-electric ram machines (EM, AE, AC, ACIES, etc.); Vipros with 18p controller; Apelio with 160iL controller
Euromac
- Compatibility condition
- MTX auto-index machines shipped after March 3, 2005; ZX auto-index machines shipped after February 18, 2005
Prima Power
- Compatibility condition
- machine serial number ≥ 7.8, or serial number 7.7 with PLC software ≥ 75.11
Variants
Rolling Rib
Max. thickness: 1.50 mm stainless steel, 2.00 mm mild steel, 2.49 mm aluminum. Stock radii 2.50 and 3.00 mm; minimum radius 16 mm (material ≤1.50mm) or 20 mm (above 1.50mm).
Rolling Shear
Thickness 0.80–1.50 mm stainless steel, 0.80–2.00 mm mild steel, 0.80–2.49 mm aluminum. Virtually no burrs or witness marks, no scrap. Minimum radius 45–100 mm.
Rolling Pincher
Same thickness ranges as Rolling Shear. Creates cuts at any angle, no scrap. Minimum radius 500 mm: the largest of the four variants, suited to gentle curves or straight cuts.
Rolling Offset
Same thickness ranges as Rolling Shear. Stock offset sizes 1.50–3.00 mm; minimum radius 25 mm. Virtually no witness marks.
Prima Power compatibility depends on the machine's serial number and PLC software version: verify these before ordering. Relevant for customers who also run Prima Power machines, distributed through the affiliated company Data Consult.
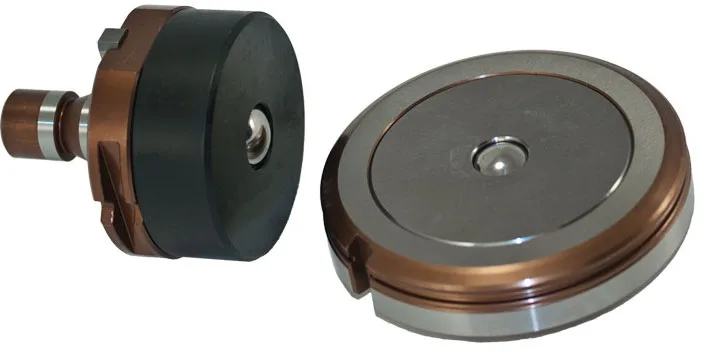
Rollerball Deburr™
Deburring on any contour · variants for Trumpf-style and Ultraform® tooling · reduces cut-hazard risk when handling sheet
Also fits: Trumpf, Euromac, Prima Power / Finn-Power
Rollerball Deburr™
Deburring on any contour · variants for Trumpf-style and Ultraform® tooling · reduces cut-hazard risk when handling sheet
Also fits: Trumpf, Euromac, Prima Power / Finn-Power
Deburring right at the press, using the same ball mechanism as Mate's Rollerball™ forming tools.
- Mechanism
- a special ball, mounted in both the upper and lower part of the tool, pushes the burr away and creates a radius on the cut edge, including on small corners
- Compatible materials
- mild steel
- stainless steel
- aluminum: no thickness limit specified by Mate
- Complete set
- three springs and a spacer (reversible on the Ultraform variant), for tensioning appropriate to the material
Variants
Trumpf-style variant
Deburrs both sides of gaps as small as 5.00 mm.
Ultraform® variant (thick turret)
Available in three tool holders: Ultraform® (fine push-button adjustment), Ultraform XT™ (manual adjustment), Ultraform FX™ (fixed length). The Rollerball Deburr insert fits into any of them.
Mate's documented workflow: the slitting operation leaves a burr on the underside of the cut, and the Rollerball Deburr™ tool is then run along the same line, pushing the burr away and creating a radius on the edge. Reduces the risk of hand cuts from handling sheet with burrs, a real safety benefit, on top of edge quality.
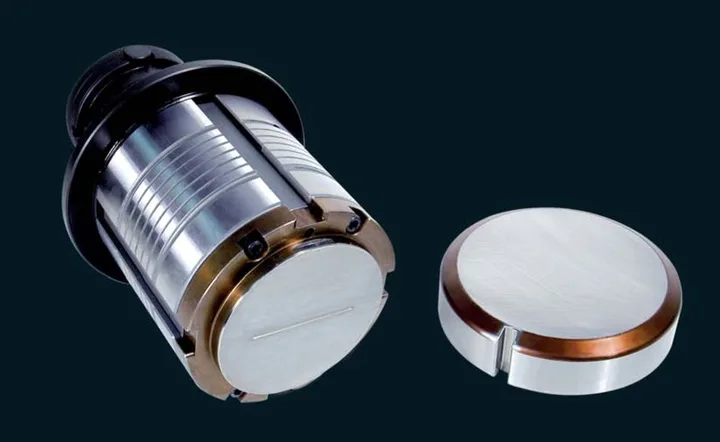
EasyBend™
Penetrating punch scores a bend line · thickness under 1.50 mm · maximum recommended length 300 mm
Also fits: Trumpf, Euromac, Prima Power / Finn-Power
EasyBend™
Penetrating punch scores a bend line · thickness under 1.50 mm · maximum recommended length 300 mm
Also fits: Trumpf, Euromac, Prima Power / Finn-Power
Eliminates a press-brake operation for small parts: the tool scores a bend line, the part is bent by hand.
- Typical applications
- target industries listed by Mate: aerospace, appliances, commercial furniture, electronics enclosures (low-stress applications), food service equipment/refrigeration, HVAC, lighting
- interlocking tabs that lock two parts together, useful for field installation or repair
- multiple or decorative bends, combined with punched louvers on the same panel
- Material thickness
- under 1.50 mm (16 gauge) as a general limit: design variations available for thicker material, on request
- Maximum recommended bend-line length
- 300 mm
- Bend angle
- the tool angle must be specified exactly at order time, matching the desired bend angle
- bends greater than 90° are not recommended
- Available configurations
- Bend Up: scores the top of the sheet
- Bend Down: scores the bottom
Parts can stay flat for shipping and be bent by hand right before final assembly: saves packing space and eliminates a separate press-brake step for small parts or short runs.
Keep in mind: Not a replacement for a press brake in volume production, or for parts with tight bend-angle accuracy requirements.
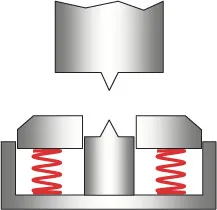
EasySnap™
Thickness 0.61–1.52 mm · maximum length 300 mm · no known tonnage restrictions
Also fits: Trumpf, Euromac, Prima Power / Finn-Power
EasySnap™
Thickness 0.61–1.52 mm · maximum length 300 mm · no known tonnage restrictions
Also fits: Trumpf, Euromac, Prima Power / Finn-Power
A controlled break line, scored on both faces of the sheet: clean manual separation, no secondary deburring step.
- Material thickness
- minimum 0.61 mm
- maximum 1.52 mm
- Maximum recommended snap-line length
- 300 mm
- Tonnage restrictions: none known, per Mate
- Compatibility: all tooling styles and station sizes, per Mate's data sheet
Practical uses documented by Mate: a temporary paint hook (the part runs through the paint line still attached, then snaps off), a press-brake back-stop locator for small parts (snapped off after the operation), and breaking a punched skeleton into smaller, easier-to-handle scrap.
Keep in mind: Will not work as intended on material thicker than the tool was designed for; on Trumpf presses it is classified as tool type 13 (embossing) in programming.
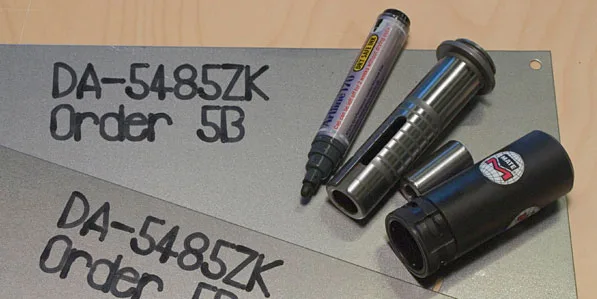
EasyMark™ 5-in-1
InkMarker™, Sheetmarker™, film cutting, center punching, and high-speed dot-matrix marking, all in one A-station tool holder
Also fits: Euromac, Prima Power / Finn-Power
EasyMark™ 5-in-1
InkMarker™, Sheetmarker™, film cutting, center punching, and high-speed dot-matrix marking, all in one A-station tool holder
Also fits: Euromac, Prima Power / Finn-Power
One tool body, five marking functions: co-developed with Prima Power.
- Origin
- Mate Precision Tooling® and Prima Power jointly developed InkMarker™, included in this kit
- Format
- a single A-station tool holder and canister, with five interchangeable configurations
- Kit contents
- dedicated tool holder and canister, InkMarker™ pen
- one brass insert, one carbide insert, two diamond inserts (120° and 150°)
- three spring types, roller ball, blank dies, and all assembly tools needed, in a dedicated protective case
Variants
InkMarker™
Writes on sheet metal with a special marker that does not dry out for two weeks or more. The mark is not physically etched (no part damage) and does not rub off unless deliberately removed.
Sheetmarker™
Etches the surface with one of two diamond inserts (120° or 150°).
Film/tape cutter
Brass insert, sharpened just enough to cut the protective film without damaging the metal underneath. Locally exposes bare metal while the rest of the sheet stays protected: for welding, spot welding, or bonding later on, for laser cutting, for a fastener to seat without the film in the way, or to prep the surface ahead of an etched mark.
Centerpoint Down
Carbide insert, combined with the machine's depth control.
High-speed dot-matrix marking
Carbide insert.
Relevant for customers who also run Prima Power machines, distributed through the affiliated company Data Consult.
Punching tools for Trumpf machines
Trumpf TruPunch and TruMatic punch presses use the Trumpf Style system, in Size 1 and Size 2. Mate divides Trumpf and Trumpf-compatible machines into four groups by alignment ring and stripper: Non-Keyed (A), Keyed (E), Rotational (H) and Minimatic (S); the exact machine model determines the group. The same tooling is also used on Boschert punch presses.
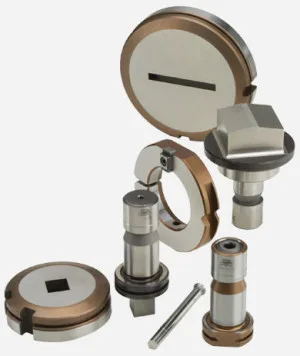
Trumpf Standard Style
Punches, dies, strippers, alignment rings · Size 1: 0.80–30.00 mm · 74.00 mm or 77.00 mm length
Trumpf Standard Style
Punches, dies, strippers, alignment rings · Size 1: 0.80–30.00 mm · 74.00 mm or 77.00 mm length
The economy tier: the full range of replacement tooling for Trumpf punch presses, with close tolerances and premium tool steels.
- Components
- punches
- dies
- strippers
- alignment rings and accessories
- Size 1
- punch range 0.80–30.00 mm
- Punches
- premium high-speed tool steel, high abrasion resistance
- 1/4° back taper and near-polished flanks
- up to 3.00 mm grind life on 6.35 mm material
- 74.00 mm standard length, 77.00 mm extended
- Stripper
- push-on urethane: quiet, non-marring even on polished aluminum
- or a hardened tool steel machine stripper, keyed for 45° settings
- Dies
- chrome air-hardened tool steel
- up to 1.50 mm grind life
- double-cut die opening
- Alignment ring
- shock-resistant tool steel, precision machined and ground
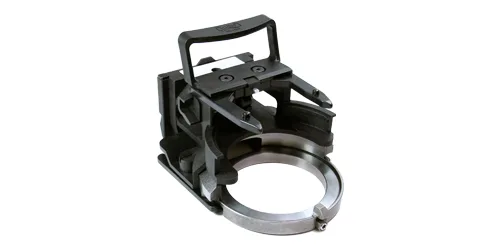
Trumpf Style Tool Cartridges
Fully OEM compatible · polymer and steel · cartridge and die plate, as an assembly or separately
Trumpf Style Tool Cartridges
Fully OEM compatible · polymer and steel · cartridge and die plate, as an assembly or separately
Tool cartridges for TRUMPF® TruPunch machines that accept the new automatic-style stripper.
- Compatibility
- TRUMPF® TruPunch machines that accept the new automatic-style stripper: 200, 500R, 600L, 1000, 2000, 2010L, 2020R, 3000, 3000L, 5000R, 6000L
- Construction
- lightweight polymer and steel design
- Supply
- cartridges and die plates, as an assembly or separately
- OEM compatibility: full
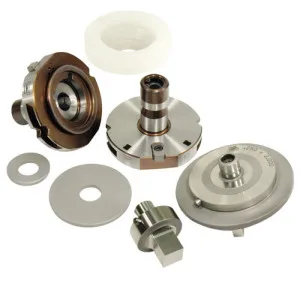
NEXT™ Insert Tooling
Interchangeable insert · precision shim system restores length · Size 40 and Size 76
NEXT™ Insert Tooling
Interchangeable insert · precision shim system restores length · Size 40 and Size 76
The premium tier of the Trumpf-compatible line: Mate's highest rating for tool life, cost, and ease of use.
- Compatibility
- Size 40: 0.80–40.00 mm punch diagonal
- Size 76: 40.03–76.36 mm
- compatible with existing conventional strippers and dies
- Insert materials
- Size 40: M4PM™ (particle-metallurgy high-speed steel), at least 50% more wear resistance than other manufacturers' conventional high-speed steel, per Mate-commissioned wear-index testing
- sizes above ~40 mm: M2 HSS
- Precision shim system
- once 0.118"(3.00mm) has been ground off the punch, a shim installed between insert and holder restores the assembly to its original overall length
- Urethane stripper (Size 40)
- push-on: positive stripping without sheet marking
- Maxima™ coating: available as an option
- Mounting: captive draw bolt + integral alignment features: no separate alignment fixture needed
- SLUG FREE® die geometry: optional
The shim system is the mechanism behind the cost savings: Mate's own cost comparison shows a single punch insert lasting as long as multiple standard punches, because the assembly length is restored after every 3.00 mm ground off, instead of consuming the entire punch. The recommended torque for the 8 mm draw bolt is 33 Nm, per Mate's dedicated installation sheet: an older figure in the general catalog (22 Nm) appears to be a conversion error and should not be used.
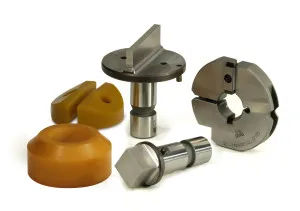
QuickLock™
Alignment key integrated on the punch · Sizes 1 and 2 · Push-On or Screw-On stripper
QuickLock™
Alignment key integrated on the punch · Sizes 1 and 2 · Push-On or Screw-On stripper
A mid tier: combines the economy of conventional Trumpf-style tooling with fast alignment through a key built into the punch.
- Compatibility
- Size 1: 0.76–30.00 mm
- Size 2: up to 76.464 mm, across four sub-ranges
- the QuickLock™ Universal Alignment Ring is also compatible with conventional (non-QuickLock) Trumpf-style Size 2 punches
- Materials
- Size 1: M4PM™ standard
- larger sizes: HSS, with Maxima™ or Nitride treatment optional
- Alignment key
- hardened and ground, built into the punch: on the shank (diagonals up to 50.80mm) or on the shoulder (above 50.80mm)
- Universal Alignment Ring
- precision-machined keyway
- precision-ground upper and lower contact surfaces
- shock-resistant tool steel
- Die regrind life
- up to 0.059"(1.50mm)
- Die opening: double-cut: opening and orientation slot cut in one operation
Urethane strippers come in two styles: Push-On (diagonals up to 50.80 mm, locks onto the punch and alignment ring) or Screw-On (for shaped punches, fixed to the punch shoulder with a screw), the choice depends on tool size and shape.
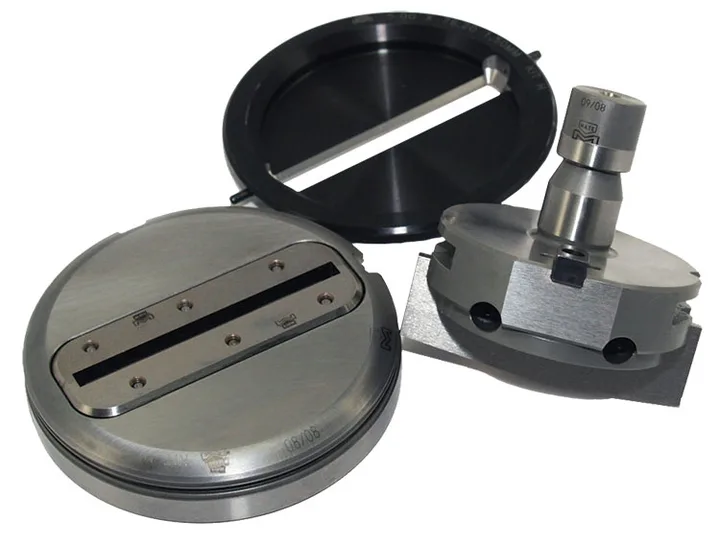
LongLife™ Slitting
M4PM™ insert · 11 die-clearance steps · real vs. nominal precision on Trumpf inserts, verified by Mate
LongLife™ Slitting
M4PM™ insert · 11 die-clearance steps · real vs. nominal precision on Trumpf inserts, verified by Mate
Mate's own "most cost-effective slitting tool solution": insert-based, fully OEM compatible.
- Compatibility
- Size 56: 19.98–55.88 mm
- Size 76: 56.01–76.08 mm
- Materials
- punch insert and die insert, both M4PM™: standard, not optional
- Die clearance
- 11 discrete steps, 0.10–0.60 mm, in 0.05 mm increments
- Available shapes
- rectangle
- oval
- dovetail
- trapezoid
- Tool holder
- with integral alignment ring (fast setup)
- or with a separate, heavy-duty alignment ring (adds manual angle-setting flexibility)
A technical detail verified directly in Mate's own catalogs: a Trumpf slitting insert at "maximum length" is actually 0.12 mm shorter than its nominal label; a part labeled 56.00 mm is actually 55.88 mm. Mate's LongLife™ tooling is sized to this real, as-built length, not the nominal label; ordering the literal nominal length triggers a special-order upcharge and is not guaranteed by Mate.
Rollerball Deburr™
Deburring on any contour · variants for Trumpf-style and Ultraform® tooling · reduces cut-hazard risk when handling sheet
Also fits: Amada, Euromac, Prima Power / Finn-Power
Rollerball Deburr™
Deburring on any contour · variants for Trumpf-style and Ultraform® tooling · reduces cut-hazard risk when handling sheet
Also fits: Amada, Euromac, Prima Power / Finn-Power
Deburring right at the press, using the same ball mechanism as Mate's Rollerball™ forming tools.
- Mechanism
- a special ball, mounted in both the upper and lower part of the tool, pushes the burr away and creates a radius on the cut edge, including on small corners
- Compatible materials
- mild steel
- stainless steel
- aluminum: no thickness limit specified by Mate
- Complete set
- three springs and a spacer (reversible on the Ultraform variant), for tensioning appropriate to the material
Variants
Trumpf-style variant
Deburrs both sides of gaps as small as 5.00 mm.
Ultraform® variant (thick turret)
Available in three tool holders: Ultraform® (fine push-button adjustment), Ultraform XT™ (manual adjustment), Ultraform FX™ (fixed length). The Rollerball Deburr insert fits into any of them.
Mate's documented workflow: the slitting operation leaves a burr on the underside of the cut, and the Rollerball Deburr™ tool is then run along the same line, pushing the burr away and creating a radius on the edge. Reduces the risk of hand cuts from handling sheet with burrs, a real safety benefit, on top of edge quality.
EasyBend™
Penetrating punch scores a bend line · thickness under 1.50 mm · maximum recommended length 300 mm
Also fits: Amada, Euromac, Prima Power / Finn-Power
EasyBend™
Penetrating punch scores a bend line · thickness under 1.50 mm · maximum recommended length 300 mm
Also fits: Amada, Euromac, Prima Power / Finn-Power
Eliminates a press-brake operation for small parts: the tool scores a bend line, the part is bent by hand.
- Typical applications
- target industries listed by Mate: aerospace, appliances, commercial furniture, electronics enclosures (low-stress applications), food service equipment/refrigeration, HVAC, lighting
- interlocking tabs that lock two parts together, useful for field installation or repair
- multiple or decorative bends, combined with punched louvers on the same panel
- Material thickness
- under 1.50 mm (16 gauge) as a general limit: design variations available for thicker material, on request
- Maximum recommended bend-line length
- 300 mm
- Bend angle
- the tool angle must be specified exactly at order time, matching the desired bend angle
- bends greater than 90° are not recommended
- Available configurations
- Bend Up: scores the top of the sheet
- Bend Down: scores the bottom
Parts can stay flat for shipping and be bent by hand right before final assembly: saves packing space and eliminates a separate press-brake step for small parts or short runs.
Keep in mind: Not a replacement for a press brake in volume production, or for parts with tight bend-angle accuracy requirements.
EasySnap™
Thickness 0.61–1.52 mm · maximum length 300 mm · no known tonnage restrictions
Also fits: Amada, Euromac, Prima Power / Finn-Power
EasySnap™
Thickness 0.61–1.52 mm · maximum length 300 mm · no known tonnage restrictions
Also fits: Amada, Euromac, Prima Power / Finn-Power
A controlled break line, scored on both faces of the sheet: clean manual separation, no secondary deburring step.
- Material thickness
- minimum 0.61 mm
- maximum 1.52 mm
- Maximum recommended snap-line length
- 300 mm
- Tonnage restrictions: none known, per Mate
- Compatibility: all tooling styles and station sizes, per Mate's data sheet
Practical uses documented by Mate: a temporary paint hook (the part runs through the paint line still attached, then snaps off), a press-brake back-stop locator for small parts (snapped off after the operation), and breaking a punched skeleton into smaller, easier-to-handle scrap.
Keep in mind: Will not work as intended on material thicker than the tool was designed for; on Trumpf presses it is classified as tool type 13 (embossing) in programming.
Punching tools for Euromac machines
Euromac thick turret punch presses use the Mate Thick Turret system, on standard stations A–E. For the Euromac FMTE6 and FMTE10 multi-tool holders there is XMT™, the only tooling designed specifically for Euromac presses, for which Mate states OEM status.
UltraTEC®
Materials and hardening · tool-free "click" length adjustment · Heavy Duty, Fully Guided, and Ultra Light variants
Also fits: Amada, Prima Power / Finn-Power
UltraTEC®
Materials and hardening · tool-free "click" length adjustment · Heavy Duty, Fully Guided, and Ultra Light variants
Also fits: Amada, Prima Power / Finn-Power
The flagship of the Thick Turret line: Mate's own comparison chart rates it highest on overall value, cost, and regrind life.
- Available stations
- A (1/2")
- B (1-1/4")
- C (2")
- D (3-1/2")
- E (4-1/2")
- Punch materials
- premium high-speed steel (HSS)
- M4PM™ optional, A and B stations: particle metallurgy, with 100% more wear resistance and 50% more toughness than conventional tool steel, and twice the interval between regrinds in customer trials, per Mate
- Max. material thickness recommended by Mate (standard system)
- aluminum 3.99 mm
- mild steel 3.99 mm
- stainless 2.90 mm (stations A–D)
- Extra regrind life vs. Original Style
- 0.118"(3.00mm) on A/B stations
- 0.212"(5.38mm) on C/D/E stations
- Usable regrind life, comparative example
- station B, 1.50 mm material, 3.00 mm die penetration: 0.408"(10.36mm) with Ultra® stripper, vs. 0.170"(4.32mm) with Original Style stripper
- stations C/D/E, same conditions: 0.512"(13.00mm) with Ultra® stripper
- "Click" length adjustment
- 0.006"(0.15mm)/click on station A
- 0.008"(0.20mm)/click on stations B/C/D/E
- no shims or separate tools
- Back taper
- 1/4° + near-polished flanks: reduces friction and galling
- Lubrication
- internal and external spiral grooves
- Guides
- hardened, ground: reduce turret bore wear
- Maxima™ coating
- available as an option: zirconium titanium nitride (ZrTiN), recommended for 3000- and 5000-series aluminum, galvanized sheet, stainless steel, and materials where lubricant can't be used; Mate cites real field tests with 2 to 10 times longer tool life
- SLUG FREE® die regrind life
- up to 0.125"(3.20mm)
- SLUG FREE® dies: standard: eliminates slug pulling, reduces tool breakage, improves hole quality
- Interchangeable with existing OEM inventory
Compatibility and dimensions
Max. punch diameter/diagonal by station (same base geometry for standard Ultra TEC®, Ultra XT™, and Original Style punches).
| Station | Max. punch diameter/diagonal | Max. die size (incl. clearance) |
|---|---|---|
| A (1/2") | 0.500"(12.70mm) | 0.559"(14.19mm) |
| B (1-1/4") | 1.250"(31.75mm) | 1.309"(33.24mm) |
| C (2") | 2.000"(50.80mm) | 2.054"(52.17mm) |
| D (3-1/2") | 3.500"(88.90mm) | 3.554"(90.27mm) |
| E (4-1/2") | 4.500"(114.30mm) | not specified |
A (1/2")
- Max. punch diameter/diagonal
- 0.500"(12.70mm)
- Max. die size (incl. clearance)
- 0.559"(14.19mm)
B (1-1/4")
- Max. punch diameter/diagonal
- 1.250"(31.75mm)
- Max. die size (incl. clearance)
- 1.309"(33.24mm)
C (2")
- Max. punch diameter/diagonal
- 2.000"(50.80mm)
- Max. die size (incl. clearance)
- 2.054"(52.17mm)
D (3-1/2")
- Max. punch diameter/diagonal
- 3.500"(88.90mm)
- Max. die size (incl. clearance)
- 3.554"(90.27mm)
E (4-1/2")
- Max. punch diameter/diagonal
- 4.500"(114.30mm)
- Max. die size (incl. clearance)
- not specified
Variants
Ultra TEC® Heavy Duty
For thicker material or noise reduction: recommended from 0.118"(3.00mm) material thickness up. Thicker-wall construction (1° back taper per side, vs. 1/4° standard), heavy-duty springs on the B station, rooftop shear available on B/C/D stations. Minimum tool size: 0.250"(6.35mm). Max. thickness recommended in the Heavy Duty variant: aluminum 6.35 mm on A/B stations and 8.00 mm on C/D, mild steel 4.57 mm on station A and 6.35 mm on B/C/D, stainless 3.99 mm on station A and 4.57 mm on B/C/D.
Ultra TEC® Fully Guided
The punch is held rigid at two extreme points (tip and back) to prevent lateral movement. Stripper clearance to the punch is 0.03 mm (vs. 0.06 mm standard): tighter guiding for hole accuracy and longer tool life. Available on B/C/D stations, with 0.008"(0.20mm) "click" adjustment.
- Slitting / Clamp Clearing variant (D, E stations): strippers allow punching as close as 15 mm from an upward-formed edge, dies as close as 20 mm from a downward-formed edge, without repositioning work-holder clamps.
Ultra Light™
Reduced-force canisters for thin, decorative, or reflective material: reduces sheet marking and noise (Mate states up to 10 dB reduction). A-station canisters apply 70% of standard Ultra TEC stripping force, B-station canisters 60%. Available on A/B/C/D/E stations.
Ultra TEC® punches are fully interchangeable with existing OEM tooling inventories (Wilson HP™/HP2™/WLS®, Amada Standard, Amada ABS, Amada Z-Standard/Z-ABS, Amada NEX, Wilson Nisshinbo Multi Tool, and others), per Mate's own compatibility matrix.
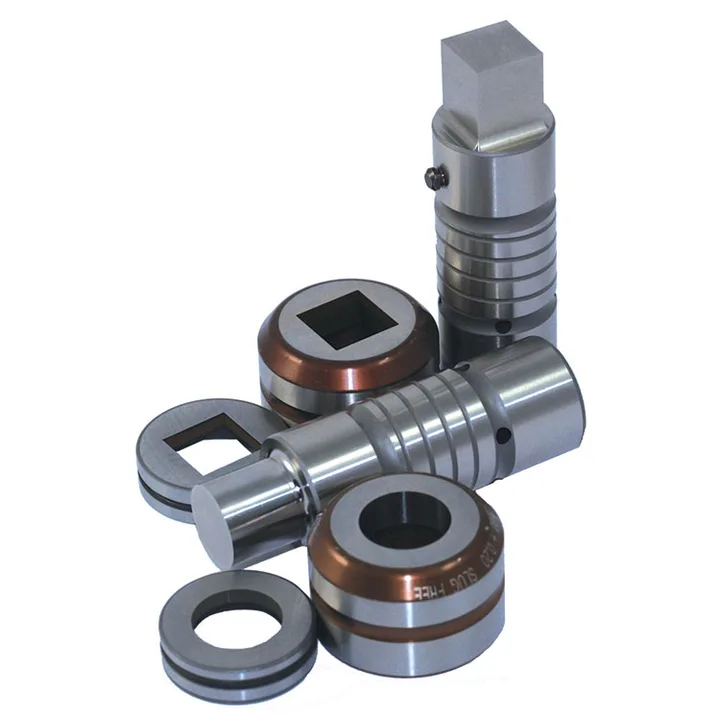
XMT™ Tooling System
Adjustable punch, up to 3× regrind life · FMTE6 and FMTE10 stations · tight 0.04–0.06 mm clearance
XMT™ Tooling System
Adjustable punch, up to 3× regrind life · FMTE6 and FMTE10 stations · tight 0.04–0.06 mm clearance
The only tooling designed specifically for Euromac™ punch presses: Mate states OEM status for Euromac.
- Compatibility
- Euromac FMTE6 and FMTE10 multi-tool punch holders
- the adjustable XMT12.7A variant: fully compatible with FMTE10 units manufactured from June 2012 on
- on older FMTE10 models: compatible with only 4 of the 10 keyed stations
- Available sizes
- XMT 12.7 mm (standard and adjustable)
- XMT 24 mm (standard and adjustable)
- Max. material thickness recommended by Mate
- aluminum 5.00 mm
- mild steel 5.00 mm
- stainless 2.49 mm (both sizes, 12.7 and 24 mm)
- Materials
- premium high-speed steel (punch)
- hardened, aircraft-grade alloy steel punch head (adjustable variants)
- Adjustable punch
- rotating the head changes the overall length, without removing the tool from the holder
- one full rotation = 1.25 mm (XMT12.7A) or 1.00 mm (XMT24A)
- Mate states up to 3 times more regrind life than a fixed punch, and up to 9.00 mm total regrind life (varies with material)
- Stripper clearance
- 0.04 mm for shapes
- 0.06 mm for rounds: tight guiding
- SLUG FREE® die regrind life
- 0.059"(1.50mm)
- Available coatings
- SuperMax™
- Maxima™
- Nitride: for extreme applications
XMT™ and MT™ tooling are not interchangeable: XMT™ is specific to Euromac FMTE6/FMTE10 holders, MT™ is the general-purpose line for other Mate multi-tool holders. Confirm your holder model before ordering.
MXC™
100% compatible with Wilson HP™/HP™ WLS®/HP™ ABS · DuraSteel™ steel · full dimension table
Also fits: Amada, Prima Power / Finn-Power
MXC™
100% compatible with Wilson HP™/HP™ WLS®/HP™ ABS · DuraSteel™ steel · full dimension table
Also fits: Amada, Prima Power / Finn-Power
"The superior alternative" for Wilson HP™ tooling users: 100% compatible, with the option to fit Ultra TEC®/Ultra XT™ guides as well.
- Compatibility
- 100% with Wilson HP™, HP™ WLS®, HP™ ABS (formerly Series 90®)
- fits Ultra TEC®/Ultra XT™ guides with an adapter or pin swap
- Materials
- DuraSteel™: high-speed steel with increased vanadium and tungsten content, 100% longer between regrinds than conventional tool steel
- Maxima™ coating
- available as an option: zirconium titanium nitride (ZrTiN), recommended for 3000- and 5000-series aluminum, galvanized sheet, stainless steel, and materials where lubricant can't be used; Mate cites real field tests with 2 to 10 times longer tool life
- Punch orientation
- hardened double-D key
- SLUG FREE® dies: standard: eliminates slug pulling, reduces tool breakage, improves hole quality
Compatibility and dimensions
Critical dimensions, verbatim from Mate's technical data sheet (mxc-tooling-system.pdf).
| Station | Max. punch diagonal | Overall length | SBR |
|---|---|---|---|
| A | 0.500"(12.70mm) | 4.640"(117.86mm) | 0.740"(18.80mm) |
| B | 1.250"(31.75mm) | 3.957"(100.51mm) | 0.740"(18.80mm) |
| C | 2.000"(50.80mm) | 2.360"(59.94mm) | 1.004"(25.50mm) |
| D | 3.500"(88.90mm) | 2.360"(59.94mm) | 1.004"(25.50mm) |
| E | 4.500"(114.30mm) | 2.360"(59.94mm) | 1.004"(25.50mm) |
A
- Max. punch diagonal
- 0.500"(12.70mm)
- Overall length
- 4.640"(117.86mm)
- SBR
- 0.740"(18.80mm)
B
- Max. punch diagonal
- 1.250"(31.75mm)
- Overall length
- 3.957"(100.51mm)
- SBR
- 0.740"(18.80mm)
C
- Max. punch diagonal
- 2.000"(50.80mm)
- Overall length
- 2.360"(59.94mm)
- SBR
- 1.004"(25.50mm)
D
- Max. punch diagonal
- 3.500"(88.90mm)
- Overall length
- 2.360"(59.94mm)
- SBR
- 1.004"(25.50mm)
E
- Max. punch diagonal
- 4.500"(114.30mm)
- Overall length
- 2.360"(59.94mm)
- SBR
- 1.004"(25.50mm)
Market note: on A/B stations, MXC punch availability may be restricted in certain countries for patent licensing reasons (per a list Mate publishes, covering several EU and North American markets). Romania does not appear on that list, but we recommend confirming directly with Mate before ordering.
Keep in mind: Fitting MXC C/D/E punches into Ultra TEC®/Ultra ABS® guides requires a dedicated HP™ adapter; shaped MXC ABS Style B-station punches cannot be adapted to Ultra XT™ guides: Ultra TEC only.
Ultraform®
Three tiers: push-button adjustment, manual adjustment, fixed length · inserts interchangeable across all three · B–E stations
Also fits: Amada, Prima Power / Finn-Power
Ultraform®
Three tiers: push-button adjustment, manual adjustment, fixed length · inserts interchangeable across all three · B–E stations
Also fits: Amada, Prima Power / Finn-Power
An adjustable-length tool holder with interchangeable inserts: buy one holder, swap only the insert for each form.
- Available stations
- B (1-1/4")
- C (2")
- D (3-1/2")
- E (4-1/2")
- Adjustment below the shoulder
- maintains the ram-to-tool gap at top of stroke: eliminates the risk of the ram striking the tool and damaging the turret
- Standard angle settings
- 0°
- 90°
- 180°
- 270°
- Guides
- hardened, with lubrication grooves
- Insert interchangeability: every insert works in any of the three holders: Ultraform®, Ultraform XT™, Ultraform FX™
Variants
Ultraform® (top tier)
Push-button length adjustment, no disassembly, in 0.05 mm increments: the finest adjustment of the three. Internal and external lubrication channels, compatible with most punch press lubrication systems.
Ultraform XT™ (mid tier)
Manual adjustment: loosen the screws, turn the punch head to the desired length. External lubrication grooves only; compatibility with the machine's lubrication system is optional, not built in.
Ultraform FX™ (fixed length)
For machines with precision stroke control at the machine level: eliminates the need for tool-side length adjustment. Not a weaker option, but the right tool for machines with their own stroke control.
The Ultraform® holder works as a platform for several Mate tools, not just forming inserts: the same B-station holders accept the Rollerball Deburr™ insert (deburring at the press), the Sheetmarker™ marking tool, and the Rollerball™ insert, which in an Ultraform® holder gains fine form-depth adjustment even on machines without precise stroke control. One holder already on hand covers several operations this way.
Keep in mind: Original Style forming tools (B station only, no interchangeable inserts) are dedicated to a single material-thickness-machine combination: moving them to another machine can damage the tool or the press. For any application where the tool will be reused across configurations, the Ultraform® family is the right choice.
Roller Solutions™
Four variants: ribbing, shearing, angled cutting, offsetting · strict compatibility with servo/auto-index machines
Also fits: Amada, Prima Power / Finn-Power
Roller Solutions™
Four variants: ribbing, shearing, angled cutting, offsetting · strict compatibility with servo/auto-index machines
Also fits: Amada, Prima Power / Finn-Power
An alternative to progressive (multi-hit) forming: runs at table travel speed, no separate secondary operations.
- Operating principle
- runs at speed equal to programmed table travel: does not slow the machine down, unlike progressive forming
- works through auto-indexing, can follow any contour
- features can start or end anywhere on the sheet
- Available station
- B (1-1/4") only
Compatibility and dimensions
Machine compatibility: a strict technical requirement (servo/auto-index motion control), not just a mechanical fit.
| Brand | Compatibility condition |
|---|---|
| Amada | servo-electric ram machines (EM, AE, AC, ACIES, etc.); Vipros with 18p controller; Apelio with 160iL controller |
| Euromac | MTX auto-index machines shipped after March 3, 2005; ZX auto-index machines shipped after February 18, 2005 |
| Prima Power | machine serial number ≥ 7.8, or serial number 7.7 with PLC software ≥ 75.11 |
Amada
- Compatibility condition
- servo-electric ram machines (EM, AE, AC, ACIES, etc.); Vipros with 18p controller; Apelio with 160iL controller
Euromac
- Compatibility condition
- MTX auto-index machines shipped after March 3, 2005; ZX auto-index machines shipped after February 18, 2005
Prima Power
- Compatibility condition
- machine serial number ≥ 7.8, or serial number 7.7 with PLC software ≥ 75.11
Variants
Rolling Rib
Max. thickness: 1.50 mm stainless steel, 2.00 mm mild steel, 2.49 mm aluminum. Stock radii 2.50 and 3.00 mm; minimum radius 16 mm (material ≤1.50mm) or 20 mm (above 1.50mm).
Rolling Shear
Thickness 0.80–1.50 mm stainless steel, 0.80–2.00 mm mild steel, 0.80–2.49 mm aluminum. Virtually no burrs or witness marks, no scrap. Minimum radius 45–100 mm.
Rolling Pincher
Same thickness ranges as Rolling Shear. Creates cuts at any angle, no scrap. Minimum radius 500 mm: the largest of the four variants, suited to gentle curves or straight cuts.
Rolling Offset
Same thickness ranges as Rolling Shear. Stock offset sizes 1.50–3.00 mm; minimum radius 25 mm. Virtually no witness marks.
Prima Power compatibility depends on the machine's serial number and PLC software version: verify these before ordering. Relevant for customers who also run Prima Power machines, distributed through the affiliated company Data Consult.
Rollerball Deburr™
Deburring on any contour · variants for Trumpf-style and Ultraform® tooling · reduces cut-hazard risk when handling sheet
Also fits: Amada, Trumpf, Prima Power / Finn-Power
Rollerball Deburr™
Deburring on any contour · variants for Trumpf-style and Ultraform® tooling · reduces cut-hazard risk when handling sheet
Also fits: Amada, Trumpf, Prima Power / Finn-Power
Deburring right at the press, using the same ball mechanism as Mate's Rollerball™ forming tools.
- Mechanism
- a special ball, mounted in both the upper and lower part of the tool, pushes the burr away and creates a radius on the cut edge, including on small corners
- Compatible materials
- mild steel
- stainless steel
- aluminum: no thickness limit specified by Mate
- Complete set
- three springs and a spacer (reversible on the Ultraform variant), for tensioning appropriate to the material
Variants
Trumpf-style variant
Deburrs both sides of gaps as small as 5.00 mm.
Ultraform® variant (thick turret)
Available in three tool holders: Ultraform® (fine push-button adjustment), Ultraform XT™ (manual adjustment), Ultraform FX™ (fixed length). The Rollerball Deburr insert fits into any of them.
Mate's documented workflow: the slitting operation leaves a burr on the underside of the cut, and the Rollerball Deburr™ tool is then run along the same line, pushing the burr away and creating a radius on the edge. Reduces the risk of hand cuts from handling sheet with burrs, a real safety benefit, on top of edge quality.
EasyBend™
Penetrating punch scores a bend line · thickness under 1.50 mm · maximum recommended length 300 mm
Also fits: Amada, Trumpf, Prima Power / Finn-Power
EasyBend™
Penetrating punch scores a bend line · thickness under 1.50 mm · maximum recommended length 300 mm
Also fits: Amada, Trumpf, Prima Power / Finn-Power
Eliminates a press-brake operation for small parts: the tool scores a bend line, the part is bent by hand.
- Typical applications
- target industries listed by Mate: aerospace, appliances, commercial furniture, electronics enclosures (low-stress applications), food service equipment/refrigeration, HVAC, lighting
- interlocking tabs that lock two parts together, useful for field installation or repair
- multiple or decorative bends, combined with punched louvers on the same panel
- Material thickness
- under 1.50 mm (16 gauge) as a general limit: design variations available for thicker material, on request
- Maximum recommended bend-line length
- 300 mm
- Bend angle
- the tool angle must be specified exactly at order time, matching the desired bend angle
- bends greater than 90° are not recommended
- Available configurations
- Bend Up: scores the top of the sheet
- Bend Down: scores the bottom
Parts can stay flat for shipping and be bent by hand right before final assembly: saves packing space and eliminates a separate press-brake step for small parts or short runs.
Keep in mind: Not a replacement for a press brake in volume production, or for parts with tight bend-angle accuracy requirements.
EasySnap™
Thickness 0.61–1.52 mm · maximum length 300 mm · no known tonnage restrictions
Also fits: Amada, Trumpf, Prima Power / Finn-Power
EasySnap™
Thickness 0.61–1.52 mm · maximum length 300 mm · no known tonnage restrictions
Also fits: Amada, Trumpf, Prima Power / Finn-Power
A controlled break line, scored on both faces of the sheet: clean manual separation, no secondary deburring step.
- Material thickness
- minimum 0.61 mm
- maximum 1.52 mm
- Maximum recommended snap-line length
- 300 mm
- Tonnage restrictions: none known, per Mate
- Compatibility: all tooling styles and station sizes, per Mate's data sheet
Practical uses documented by Mate: a temporary paint hook (the part runs through the paint line still attached, then snaps off), a press-brake back-stop locator for small parts (snapped off after the operation), and breaking a punched skeleton into smaller, easier-to-handle scrap.
Keep in mind: Will not work as intended on material thicker than the tool was designed for; on Trumpf presses it is classified as tool type 13 (embossing) in programming.
EasyMark™ 5-in-1
InkMarker™, Sheetmarker™, film cutting, center punching, and high-speed dot-matrix marking, all in one A-station tool holder
Also fits: Amada, Prima Power / Finn-Power
EasyMark™ 5-in-1
InkMarker™, Sheetmarker™, film cutting, center punching, and high-speed dot-matrix marking, all in one A-station tool holder
Also fits: Amada, Prima Power / Finn-Power
One tool body, five marking functions: co-developed with Prima Power.
- Origin
- Mate Precision Tooling® and Prima Power jointly developed InkMarker™, included in this kit
- Format
- a single A-station tool holder and canister, with five interchangeable configurations
- Kit contents
- dedicated tool holder and canister, InkMarker™ pen
- one brass insert, one carbide insert, two diamond inserts (120° and 150°)
- three spring types, roller ball, blank dies, and all assembly tools needed, in a dedicated protective case
Variants
InkMarker™
Writes on sheet metal with a special marker that does not dry out for two weeks or more. The mark is not physically etched (no part damage) and does not rub off unless deliberately removed.
Sheetmarker™
Etches the surface with one of two diamond inserts (120° or 150°).
Film/tape cutter
Brass insert, sharpened just enough to cut the protective film without damaging the metal underneath. Locally exposes bare metal while the rest of the sheet stays protected: for welding, spot welding, or bonding later on, for laser cutting, for a fastener to seat without the film in the way, or to prep the surface ahead of an etched mark.
Centerpoint Down
Carbide insert, combined with the machine's depth control.
High-speed dot-matrix marking
Carbide insert.
Relevant for customers who also run Prima Power machines, distributed through the affiliated company Data Consult.
Punching tools for LVD Strippit machines
LVD Strippit machines are thin turret punch presses, with different tooling from thick turret machines. Mate has two lines for them: Strippit Style, in the original station formats, and Xcel™, the precision system with quick length adjustment.
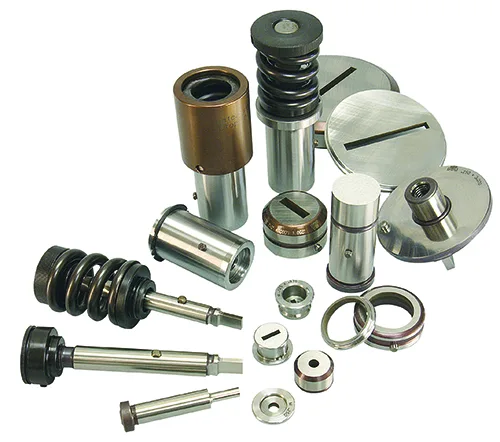
Strippit Style
1/2" Snap-Apart, 5/8" Drop-In, 1-1/4" Full Body, 3-1/2" stations · MTG™ Multi Tool · DuraSteel™ punches
Strippit Style
1/2" Snap-Apart, 5/8" Drop-In, 1-1/4" Full Body, 3-1/2" stations · MTG™ Multi Tool · DuraSteel™ punches
Thin Turret tooling for LVD Strippit punch presses, in the original station formats.
- Stations
- 1/2" Snap-Apart
- 5/8" Drop-In
- 1-1/4" Full Body
- 3-1/2"
- MTG™ Multi Tool, 3 station (1.250")
- MTG™ Multi Tool, 8 station (0.500")
- Punches
- DuraSteel™ on every station
- 1-1/4" station: 1/4° back taper against friction and galling
- 5/8" station: hardened double-D key for precise orientation of shapes
- Strippers
- toughened, for long service life
- rounded edges, no sheet marking
- 5/8" Drop-In station
- self-contained, pre-loaded spring and hardened guide in one assembly
- Slug Free® dies: on every station
- Compatible with existing inventory
Xcel™
1-1/4" and 2" stations · 3-1/2" guide assembly for Strippit · push-button adjustment in 0.20 mm steps
Xcel™
1-1/4" and 2" stations · 3-1/2" guide assembly for Strippit · push-button adjustment in 0.20 mm steps
Mate's precision system for thin turret punch presses: quick tool changes and length adjustment without shims.
- Stations
- 1-1/4"
- 2"
- 3-1/2" guide assembly for Strippit
- Length adjustment
- push-button, without disassembly, in 0.20 mm increments
- no shims or tools required
- Punch
- DuraSteel™, high hardness and toughness
- hardened double-D key
- 1/4° back taper and near-polished flanks
- Maxima® coating available for extreme applications
- Canister
- self-contained, pre-loaded spring pack for consistent stripping pressure
- Accessories
- maintenance fixture for thin turret tooling
- Multi Tool systems
- Slug Free® dies
- Compatible with existing inventory
Mate presents Xcel™ for LVD Strippit and Amada thin turret punch presses.
Punching tools for Prima Power / Finn-Power machines
Prima Power (formerly Finn-Power) punch presses use the Mate Thick Turret system, on stations A–E. Some forming tools carry conditions tied to the machine series and software version, noted on each card. Through our affiliated company, Data Consult, we also distribute Prima Power machines.
UltraTEC®
Materials and hardening · tool-free "click" length adjustment · Heavy Duty, Fully Guided, and Ultra Light variants
Also fits: Amada, Euromac
UltraTEC®
Materials and hardening · tool-free "click" length adjustment · Heavy Duty, Fully Guided, and Ultra Light variants
Also fits: Amada, Euromac
The flagship of the Thick Turret line: Mate's own comparison chart rates it highest on overall value, cost, and regrind life.
- Available stations
- A (1/2")
- B (1-1/4")
- C (2")
- D (3-1/2")
- E (4-1/2")
- Punch materials
- premium high-speed steel (HSS)
- M4PM™ optional, A and B stations: particle metallurgy, with 100% more wear resistance and 50% more toughness than conventional tool steel, and twice the interval between regrinds in customer trials, per Mate
- Max. material thickness recommended by Mate (standard system)
- aluminum 3.99 mm
- mild steel 3.99 mm
- stainless 2.90 mm (stations A–D)
- Extra regrind life vs. Original Style
- 0.118"(3.00mm) on A/B stations
- 0.212"(5.38mm) on C/D/E stations
- Usable regrind life, comparative example
- station B, 1.50 mm material, 3.00 mm die penetration: 0.408"(10.36mm) with Ultra® stripper, vs. 0.170"(4.32mm) with Original Style stripper
- stations C/D/E, same conditions: 0.512"(13.00mm) with Ultra® stripper
- "Click" length adjustment
- 0.006"(0.15mm)/click on station A
- 0.008"(0.20mm)/click on stations B/C/D/E
- no shims or separate tools
- Back taper
- 1/4° + near-polished flanks: reduces friction and galling
- Lubrication
- internal and external spiral grooves
- Guides
- hardened, ground: reduce turret bore wear
- Maxima™ coating
- available as an option: zirconium titanium nitride (ZrTiN), recommended for 3000- and 5000-series aluminum, galvanized sheet, stainless steel, and materials where lubricant can't be used; Mate cites real field tests with 2 to 10 times longer tool life
- SLUG FREE® die regrind life
- up to 0.125"(3.20mm)
- SLUG FREE® dies: standard: eliminates slug pulling, reduces tool breakage, improves hole quality
- Interchangeable with existing OEM inventory
Compatibility and dimensions
Max. punch diameter/diagonal by station (same base geometry for standard Ultra TEC®, Ultra XT™, and Original Style punches).
| Station | Max. punch diameter/diagonal | Max. die size (incl. clearance) |
|---|---|---|
| A (1/2") | 0.500"(12.70mm) | 0.559"(14.19mm) |
| B (1-1/4") | 1.250"(31.75mm) | 1.309"(33.24mm) |
| C (2") | 2.000"(50.80mm) | 2.054"(52.17mm) |
| D (3-1/2") | 3.500"(88.90mm) | 3.554"(90.27mm) |
| E (4-1/2") | 4.500"(114.30mm) | not specified |
A (1/2")
- Max. punch diameter/diagonal
- 0.500"(12.70mm)
- Max. die size (incl. clearance)
- 0.559"(14.19mm)
B (1-1/4")
- Max. punch diameter/diagonal
- 1.250"(31.75mm)
- Max. die size (incl. clearance)
- 1.309"(33.24mm)
C (2")
- Max. punch diameter/diagonal
- 2.000"(50.80mm)
- Max. die size (incl. clearance)
- 2.054"(52.17mm)
D (3-1/2")
- Max. punch diameter/diagonal
- 3.500"(88.90mm)
- Max. die size (incl. clearance)
- 3.554"(90.27mm)
E (4-1/2")
- Max. punch diameter/diagonal
- 4.500"(114.30mm)
- Max. die size (incl. clearance)
- not specified
Variants
Ultra TEC® Heavy Duty
For thicker material or noise reduction: recommended from 0.118"(3.00mm) material thickness up. Thicker-wall construction (1° back taper per side, vs. 1/4° standard), heavy-duty springs on the B station, rooftop shear available on B/C/D stations. Minimum tool size: 0.250"(6.35mm). Max. thickness recommended in the Heavy Duty variant: aluminum 6.35 mm on A/B stations and 8.00 mm on C/D, mild steel 4.57 mm on station A and 6.35 mm on B/C/D, stainless 3.99 mm on station A and 4.57 mm on B/C/D.
Ultra TEC® Fully Guided
The punch is held rigid at two extreme points (tip and back) to prevent lateral movement. Stripper clearance to the punch is 0.03 mm (vs. 0.06 mm standard): tighter guiding for hole accuracy and longer tool life. Available on B/C/D stations, with 0.008"(0.20mm) "click" adjustment.
- Slitting / Clamp Clearing variant (D, E stations): strippers allow punching as close as 15 mm from an upward-formed edge, dies as close as 20 mm from a downward-formed edge, without repositioning work-holder clamps.
Ultra Light™
Reduced-force canisters for thin, decorative, or reflective material: reduces sheet marking and noise (Mate states up to 10 dB reduction). A-station canisters apply 70% of standard Ultra TEC stripping force, B-station canisters 60%. Available on A/B/C/D/E stations.
Ultra TEC® punches are fully interchangeable with existing OEM tooling inventories (Wilson HP™/HP2™/WLS®, Amada Standard, Amada ABS, Amada Z-Standard/Z-ABS, Amada NEX, Wilson Nisshinbo Multi Tool, and others), per Mate's own compatibility matrix.
MXC™
100% compatible with Wilson HP™/HP™ WLS®/HP™ ABS · DuraSteel™ steel · full dimension table
Also fits: Amada, Euromac
MXC™
100% compatible with Wilson HP™/HP™ WLS®/HP™ ABS · DuraSteel™ steel · full dimension table
Also fits: Amada, Euromac
"The superior alternative" for Wilson HP™ tooling users: 100% compatible, with the option to fit Ultra TEC®/Ultra XT™ guides as well.
- Compatibility
- 100% with Wilson HP™, HP™ WLS®, HP™ ABS (formerly Series 90®)
- fits Ultra TEC®/Ultra XT™ guides with an adapter or pin swap
- Materials
- DuraSteel™: high-speed steel with increased vanadium and tungsten content, 100% longer between regrinds than conventional tool steel
- Maxima™ coating
- available as an option: zirconium titanium nitride (ZrTiN), recommended for 3000- and 5000-series aluminum, galvanized sheet, stainless steel, and materials where lubricant can't be used; Mate cites real field tests with 2 to 10 times longer tool life
- Punch orientation
- hardened double-D key
- SLUG FREE® dies: standard: eliminates slug pulling, reduces tool breakage, improves hole quality
Compatibility and dimensions
Critical dimensions, verbatim from Mate's technical data sheet (mxc-tooling-system.pdf).
| Station | Max. punch diagonal | Overall length | SBR |
|---|---|---|---|
| A | 0.500"(12.70mm) | 4.640"(117.86mm) | 0.740"(18.80mm) |
| B | 1.250"(31.75mm) | 3.957"(100.51mm) | 0.740"(18.80mm) |
| C | 2.000"(50.80mm) | 2.360"(59.94mm) | 1.004"(25.50mm) |
| D | 3.500"(88.90mm) | 2.360"(59.94mm) | 1.004"(25.50mm) |
| E | 4.500"(114.30mm) | 2.360"(59.94mm) | 1.004"(25.50mm) |
A
- Max. punch diagonal
- 0.500"(12.70mm)
- Overall length
- 4.640"(117.86mm)
- SBR
- 0.740"(18.80mm)
B
- Max. punch diagonal
- 1.250"(31.75mm)
- Overall length
- 3.957"(100.51mm)
- SBR
- 0.740"(18.80mm)
C
- Max. punch diagonal
- 2.000"(50.80mm)
- Overall length
- 2.360"(59.94mm)
- SBR
- 1.004"(25.50mm)
D
- Max. punch diagonal
- 3.500"(88.90mm)
- Overall length
- 2.360"(59.94mm)
- SBR
- 1.004"(25.50mm)
E
- Max. punch diagonal
- 4.500"(114.30mm)
- Overall length
- 2.360"(59.94mm)
- SBR
- 1.004"(25.50mm)
Market note: on A/B stations, MXC punch availability may be restricted in certain countries for patent licensing reasons (per a list Mate publishes, covering several EU and North American markets). Romania does not appear on that list, but we recommend confirming directly with Mate before ordering.
Keep in mind: Fitting MXC C/D/E punches into Ultra TEC®/Ultra ABS® guides requires a dedicated HP™ adapter; shaped MXC ABS Style B-station punches cannot be adapted to Ultra XT™ guides: Ultra TEC only.
MT™ Tooling System
Three sizes: 8, 16, and 24 mm · SLUG FREE® dies standard · Maxima® coating optional
Also fits: Amada
MT™ Tooling System
Three sizes: 8, 16, and 24 mm · SLUG FREE® dies standard · Maxima® coating optional
Also fits: Amada
Mate's general-purpose Multi Tool line, compatible with Mate-manufactured multi-tool assemblies.
- Available sizes
- 8 mm
- 16 mm
- 24 mm (max. punch diameter/diagonal)
- Max. material thickness recommended by Mate
- MT 8 mm: aluminum 3.99 mm, mild steel 3.00 mm, stainless 1.98 mm
- MT 24 mm: aluminum 5.00 mm, mild steel 5.00 mm, stainless 2.49 mm
- Materials
- high-speed steel (HSS) punches, resistant to edge wear
- Back taper
- 1/4° + near-polished flanks: eliminates galling
- Punch-to-stripper clearance
- tight: superior guiding
- SLUG FREE® dies: standard: eliminates slug pulling, improves hole quality
- Maxima® coating: available as an option, for extended tool life
Dedicated service tool sets (stripper/die puller, magnet pen, retrieving tool) are available for each size, plus a complete kit covering all three.
Ultraform®
Three tiers: push-button adjustment, manual adjustment, fixed length · inserts interchangeable across all three · B–E stations
Also fits: Amada, Euromac
Ultraform®
Three tiers: push-button adjustment, manual adjustment, fixed length · inserts interchangeable across all three · B–E stations
Also fits: Amada, Euromac
An adjustable-length tool holder with interchangeable inserts: buy one holder, swap only the insert for each form.
- Available stations
- B (1-1/4")
- C (2")
- D (3-1/2")
- E (4-1/2")
- Adjustment below the shoulder
- maintains the ram-to-tool gap at top of stroke: eliminates the risk of the ram striking the tool and damaging the turret
- Standard angle settings
- 0°
- 90°
- 180°
- 270°
- Guides
- hardened, with lubrication grooves
- Insert interchangeability: every insert works in any of the three holders: Ultraform®, Ultraform XT™, Ultraform FX™
Variants
Ultraform® (top tier)
Push-button length adjustment, no disassembly, in 0.05 mm increments: the finest adjustment of the three. Internal and external lubrication channels, compatible with most punch press lubrication systems.
Ultraform XT™ (mid tier)
Manual adjustment: loosen the screws, turn the punch head to the desired length. External lubrication grooves only; compatibility with the machine's lubrication system is optional, not built in.
Ultraform FX™ (fixed length)
For machines with precision stroke control at the machine level: eliminates the need for tool-side length adjustment. Not a weaker option, but the right tool for machines with their own stroke control.
The Ultraform® holder works as a platform for several Mate tools, not just forming inserts: the same B-station holders accept the Rollerball Deburr™ insert (deburring at the press), the Sheetmarker™ marking tool, and the Rollerball™ insert, which in an Ultraform® holder gains fine form-depth adjustment even on machines without precise stroke control. One holder already on hand covers several operations this way.
Keep in mind: Original Style forming tools (B station only, no interchangeable inserts) are dedicated to a single material-thickness-machine combination: moving them to another machine can damage the tool or the press. For any application where the tool will be reused across configurations, the Ultraform® family is the right choice.
Roller Solutions™
Four variants: ribbing, shearing, angled cutting, offsetting · strict compatibility with servo/auto-index machines
Also fits: Amada, Euromac
Roller Solutions™
Four variants: ribbing, shearing, angled cutting, offsetting · strict compatibility with servo/auto-index machines
Also fits: Amada, Euromac
An alternative to progressive (multi-hit) forming: runs at table travel speed, no separate secondary operations.
- Operating principle
- runs at speed equal to programmed table travel: does not slow the machine down, unlike progressive forming
- works through auto-indexing, can follow any contour
- features can start or end anywhere on the sheet
- Available station
- B (1-1/4") only
Compatibility and dimensions
Machine compatibility: a strict technical requirement (servo/auto-index motion control), not just a mechanical fit.
| Brand | Compatibility condition |
|---|---|
| Amada | servo-electric ram machines (EM, AE, AC, ACIES, etc.); Vipros with 18p controller; Apelio with 160iL controller |
| Euromac | MTX auto-index machines shipped after March 3, 2005; ZX auto-index machines shipped after February 18, 2005 |
| Prima Power | machine serial number ≥ 7.8, or serial number 7.7 with PLC software ≥ 75.11 |
Amada
- Compatibility condition
- servo-electric ram machines (EM, AE, AC, ACIES, etc.); Vipros with 18p controller; Apelio with 160iL controller
Euromac
- Compatibility condition
- MTX auto-index machines shipped after March 3, 2005; ZX auto-index machines shipped after February 18, 2005
Prima Power
- Compatibility condition
- machine serial number ≥ 7.8, or serial number 7.7 with PLC software ≥ 75.11
Variants
Rolling Rib
Max. thickness: 1.50 mm stainless steel, 2.00 mm mild steel, 2.49 mm aluminum. Stock radii 2.50 and 3.00 mm; minimum radius 16 mm (material ≤1.50mm) or 20 mm (above 1.50mm).
Rolling Shear
Thickness 0.80–1.50 mm stainless steel, 0.80–2.00 mm mild steel, 0.80–2.49 mm aluminum. Virtually no burrs or witness marks, no scrap. Minimum radius 45–100 mm.
Rolling Pincher
Same thickness ranges as Rolling Shear. Creates cuts at any angle, no scrap. Minimum radius 500 mm: the largest of the four variants, suited to gentle curves or straight cuts.
Rolling Offset
Same thickness ranges as Rolling Shear. Stock offset sizes 1.50–3.00 mm; minimum radius 25 mm. Virtually no witness marks.
Prima Power compatibility depends on the machine's serial number and PLC software version: verify these before ordering. Relevant for customers who also run Prima Power machines, distributed through the affiliated company Data Consult.
Rollerball Deburr™
Deburring on any contour · variants for Trumpf-style and Ultraform® tooling · reduces cut-hazard risk when handling sheet
Also fits: Amada, Trumpf, Euromac
Rollerball Deburr™
Deburring on any contour · variants for Trumpf-style and Ultraform® tooling · reduces cut-hazard risk when handling sheet
Also fits: Amada, Trumpf, Euromac
Deburring right at the press, using the same ball mechanism as Mate's Rollerball™ forming tools.
- Mechanism
- a special ball, mounted in both the upper and lower part of the tool, pushes the burr away and creates a radius on the cut edge, including on small corners
- Compatible materials
- mild steel
- stainless steel
- aluminum: no thickness limit specified by Mate
- Complete set
- three springs and a spacer (reversible on the Ultraform variant), for tensioning appropriate to the material
Variants
Trumpf-style variant
Deburrs both sides of gaps as small as 5.00 mm.
Ultraform® variant (thick turret)
Available in three tool holders: Ultraform® (fine push-button adjustment), Ultraform XT™ (manual adjustment), Ultraform FX™ (fixed length). The Rollerball Deburr insert fits into any of them.
Mate's documented workflow: the slitting operation leaves a burr on the underside of the cut, and the Rollerball Deburr™ tool is then run along the same line, pushing the burr away and creating a radius on the edge. Reduces the risk of hand cuts from handling sheet with burrs, a real safety benefit, on top of edge quality.
EasyBend™
Penetrating punch scores a bend line · thickness under 1.50 mm · maximum recommended length 300 mm
Also fits: Amada, Trumpf, Euromac
EasyBend™
Penetrating punch scores a bend line · thickness under 1.50 mm · maximum recommended length 300 mm
Also fits: Amada, Trumpf, Euromac
Eliminates a press-brake operation for small parts: the tool scores a bend line, the part is bent by hand.
- Typical applications
- target industries listed by Mate: aerospace, appliances, commercial furniture, electronics enclosures (low-stress applications), food service equipment/refrigeration, HVAC, lighting
- interlocking tabs that lock two parts together, useful for field installation or repair
- multiple or decorative bends, combined with punched louvers on the same panel
- Material thickness
- under 1.50 mm (16 gauge) as a general limit: design variations available for thicker material, on request
- Maximum recommended bend-line length
- 300 mm
- Bend angle
- the tool angle must be specified exactly at order time, matching the desired bend angle
- bends greater than 90° are not recommended
- Available configurations
- Bend Up: scores the top of the sheet
- Bend Down: scores the bottom
Parts can stay flat for shipping and be bent by hand right before final assembly: saves packing space and eliminates a separate press-brake step for small parts or short runs.
Keep in mind: Not a replacement for a press brake in volume production, or for parts with tight bend-angle accuracy requirements.
EasySnap™
Thickness 0.61–1.52 mm · maximum length 300 mm · no known tonnage restrictions
Also fits: Amada, Trumpf, Euromac
EasySnap™
Thickness 0.61–1.52 mm · maximum length 300 mm · no known tonnage restrictions
Also fits: Amada, Trumpf, Euromac
A controlled break line, scored on both faces of the sheet: clean manual separation, no secondary deburring step.
- Material thickness
- minimum 0.61 mm
- maximum 1.52 mm
- Maximum recommended snap-line length
- 300 mm
- Tonnage restrictions: none known, per Mate
- Compatibility: all tooling styles and station sizes, per Mate's data sheet
Practical uses documented by Mate: a temporary paint hook (the part runs through the paint line still attached, then snaps off), a press-brake back-stop locator for small parts (snapped off after the operation), and breaking a punched skeleton into smaller, easier-to-handle scrap.
Keep in mind: Will not work as intended on material thicker than the tool was designed for; on Trumpf presses it is classified as tool type 13 (embossing) in programming.
EasyMark™ 5-in-1
InkMarker™, Sheetmarker™, film cutting, center punching, and high-speed dot-matrix marking, all in one A-station tool holder
Also fits: Amada, Euromac
EasyMark™ 5-in-1
InkMarker™, Sheetmarker™, film cutting, center punching, and high-speed dot-matrix marking, all in one A-station tool holder
Also fits: Amada, Euromac
One tool body, five marking functions: co-developed with Prima Power.
- Origin
- Mate Precision Tooling® and Prima Power jointly developed InkMarker™, included in this kit
- Format
- a single A-station tool holder and canister, with five interchangeable configurations
- Kit contents
- dedicated tool holder and canister, InkMarker™ pen
- one brass insert, one carbide insert, two diamond inserts (120° and 150°)
- three spring types, roller ball, blank dies, and all assembly tools needed, in a dedicated protective case
Variants
InkMarker™
Writes on sheet metal with a special marker that does not dry out for two weeks or more. The mark is not physically etched (no part damage) and does not rub off unless deliberately removed.
Sheetmarker™
Etches the surface with one of two diamond inserts (120° or 150°).
Film/tape cutter
Brass insert, sharpened just enough to cut the protective film without damaging the metal underneath. Locally exposes bare metal while the rest of the sheet stays protected: for welding, spot welding, or bonding later on, for laser cutting, for a fastener to seat without the film in the way, or to prep the surface ahead of an etched mark.
Centerpoint Down
Carbide insert, combined with the machine's depth control.
High-speed dot-matrix marking
Carbide insert.
Relevant for customers who also run Prima Power machines, distributed through the affiliated company Data Consult.
Request a quote: Punching tools for Prima Power / Finn-Power machines
Punching tools for Salvagnini machines
Salvagnini punch presses have their own punching system, with positions by tonnage (7 t, 12 t, 26 t) rather than thick turret stations. For them Mate makes the Salvagnini Style Type III line and the P0 perforating system for small holes.
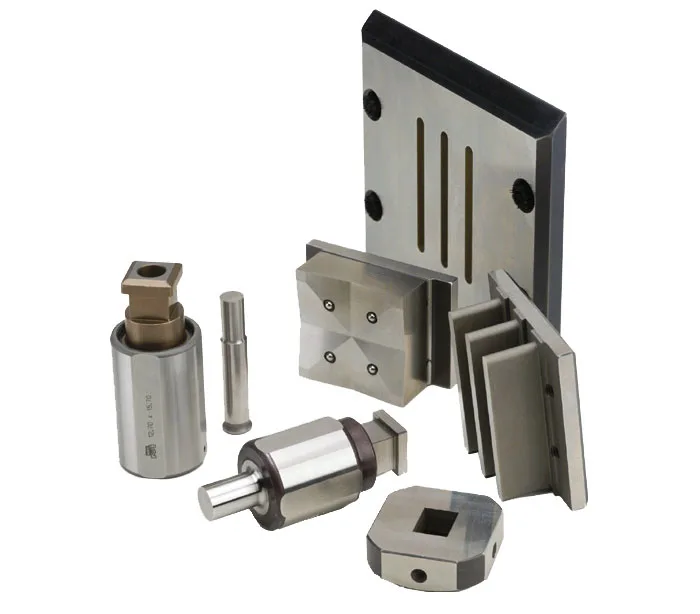
Salvagnini Style Type III
Positions 1–20, 41–76 (7 t), 30–35 (12 t), 21–24 (26 t) · powdered-metal high-speed steel · Slug Free® at no extra cost
Salvagnini Style Type III
Positions 1–20, 41–76 (7 t), 30–35 (12 t), 21–24 (26 t) · powdered-metal high-speed steel · Slug Free® at no extra cost
High-speed steel punches, dies and strippers for Salvagnini's punching system, including special shapes and forming assemblies to specification.
- Positions 1–20 and 41–76 (7 t)
- 6 mm (rounds only)
- 10.5 mm (rounds only)
- 33 mm: diagonal up to 26.00 mm, fully guided perforating assembly
- Positions 30–35 (12 t)
- 60 mm, auto-index
- Positions 21–24 (26 t)
- 70×90 (Type 70)
- 90×90 (Type 90)
- Punches
- premium powdered-metal high-speed steel: abrasion and galling resistance
- resharpening up to 4.00 mm
- punch chuck available for punch sizes of 10.5 mm and under
- Dies
- high-speed steel, in the 33 mm stations (A, B, C)
- resharpening up to 1.50 mm
- specify clearance as punch size PLUS total clearance, not per side
- Stations D, E, F
- brushes that prevent marking
- Slug Free® dies: optional on every Type III station, at no extra cost
- Special shapes: to customer specification
P0 Perforating System
Shapes up to 12.50 mm · MPM82™ powdered tool steel · fully guided stripper
P0 Perforating System
Shapes up to 12.50 mm · MPM82™ powdered tool steel · fully guided stripper
A fully guided perforating system for small holes in the 7-ton stations of Salvagnini punch presses.
- Application
- small holes in the 7-ton stations, across their full size range
- Punch size
- any shape up to 12.50 mm
- Punches
- MPM82™ powdered tool steel: wear and chipping resistance
- resharpening up to 1.49 mm
- nitride treatment, Maxima™ and SuperMax™ coatings available
- Stripper
- fully guided, supports the punch point throughout the cycle
- assembled into the upper cartridge
- Special shapes: to customer specification
Punching tools for Murata Wiedemann machines
For Murata Wiedemann punch presses, Mate is the manufacturer's OEM supplier. The range covers Marathon Plus™/Marathon® for high volumes, the 112 and 114 styles to OEM standard, and the Vulcan system.
Marathon Plus™ / Marathon®
Marathon Plus™: external quick length adjustment · Marathon®: built-in adjustable shim · 8 angle settings
Marathon Plus™ / Marathon®
Marathon Plus™: external quick length adjustment · Marathon®: built-in adjustable shim · 8 angle settings
The high-performance tier for Murata Wiedemann punch presses, built for high-volume, high-speed punching.
- Marathon Plus™
- external quick length adjustment mechanism, for very fast tool changes
- for Vectrum, Motorum and Magnum machines
- Marathon®
- built-in adjustable shim for optimum length setting
- Construction
- contained forces, reduced turret wear
- hardened and ground punch holder
- reduced travel and hardened guide: longer turret bore life
- 3-point guiding
- Stripper
- spring-loaded, holds the sheet flatter
- Angles
- 8 settings
112 Style and 114 Style
Fully OEM compatible · chrome air-hardened tool steel · Slug Free® dies with 3.00 mm grind life
112 Style and 114 Style
Fully OEM compatible · chrome air-hardened tool steel · Slug Free® dies with 3.00 mm grind life
The OEM standard for Murata Wiedemann punch presses, economy tier; Mate is Murata Wiedemann's OEM supplier.
- Punches
- fully OEM compatible
- chrome air-hardened tool steel, balancing hardness and toughness
- 1/4° back taper and near-polished flanks
- Slug Free® dies
- geometry that eliminates slug pulling
- uniform clearance radii in die corners
- up to 3.00 mm grind life
- Stress Free™ relief that distributes forces
- Fit
- OEM tolerances: correct concentricity and alignment in the machine bores
Vulcan
Stations X to L · max. punch 12.70–152.00 mm · metal stripper with lateral support
Vulcan
Stations X to L · max. punch 12.70–152.00 mm · metal stripper with lateral support
A system for Murata Wiedemann punch presses with high-speed steel punches, metal strippers and Slug Free® dies.
- Max. punch per station
- X: 12.70 mm (rounds only)
- AB: 25.00 mm (120.42 mm overall length)
- B: 25.00 mm (50.42 mm overall length)
- C: 38.00 mm · D: 51.00 mm · E: 63.50 mm
- F: 76.20 mm · G: 88.90 mm · H: 104.78 mm
- J: 120.65 mm · K: 139.70 mm · L: 152.00 mm
- Punches
- high-speed tool steel
- 1/4° back taper and near-polished flanks
- minute corner radii against chipping
- Stripper
- metal, gives lateral punch support
- superior angularity and concentricity
- Slug Free® dies
- chrome air-hardened tool steel
- precise orientation with an external pin
- up to 3.00 mm grind life
Request a quote: Punching tools for Murata Wiedemann machines
Mate systems and catalogs
Mate Precision Technologies manufactures original and replacement tooling for the main brands of CNC turret punch presses. The table below shows which Mate system fits each machine type.
| Mate tooling system | Compatible punch presses | Stations / Notes |
|---|---|---|
| Thick Turret: Ultra® (UltraTEC®, Ultra XT™, Original Style), MXC™ | Amada, Euromac, Prima Power / Finn-Power, Tailift and other thick turret presses, such as Danobat | Stations A (½"), B (1¼"), C (2"), D (3½"), E (4½") |
| AMX™ ABS | Amada with ABS clamping: assemblies and tool holders | Full compatibility with the Amada ABS system |
| Multi Tool (Ultra® IMT, MT™, XMT™) | Thick turret presses; XMT™ only for Euromac FMTE6 and FMTE10 holders | Multi-station indexing from a single turret position |
| Trumpf Style (Standard, cartridges, NEXT™, QuickLock™, LongLife™) | Trumpf TruPunch and TruMatic, Boschert | Size 1 and Size 2 |
| Thin Turret (Strippit Style, Xcel™) | LVD Strippit | Stations 1/2", 5/8", 1-1/4", 2", 3-1/2" |
| Salvagnini Style Type III, P0 perforating | Salvagnini | Positions 1–20 and 41–76 (7 t), 30–35 (12 t), 21–24 (26 t) |
| Marathon Plus™/Marathon®, 112/114 Style, Vulcan | Murata Wiedemann | Mate is an OEM supplier to Murata Wiedemann |
Thick Turret: Ultra® (UltraTEC®, Ultra XT™, Original Style), MXC™
- Compatible punch presses
- Amada, Euromac, Prima Power / Finn-Power, Tailift and other thick turret presses, such as Danobat
- Stations / Notes
- Stations A (½"), B (1¼"), C (2"), D (3½"), E (4½")
AMX™ ABS
- Compatible punch presses
- Amada with ABS clamping: assemblies and tool holders
- Stations / Notes
- Full compatibility with the Amada ABS system
Multi Tool (Ultra® IMT, MT™, XMT™)
- Compatible punch presses
- Thick turret presses; XMT™ only for Euromac FMTE6 and FMTE10 holders
- Stations / Notes
- Multi-station indexing from a single turret position
Trumpf Style (Standard, cartridges, NEXT™, QuickLock™, LongLife™)
- Compatible punch presses
- Trumpf TruPunch and TruMatic, Boschert
- Stations / Notes
- Size 1 and Size 2
Thin Turret (Strippit Style, Xcel™)
- Compatible punch presses
- LVD Strippit
- Stations / Notes
- Stations 1/2", 5/8", 1-1/4", 2", 3-1/2"
Salvagnini Style Type III, P0 perforating
- Compatible punch presses
- Salvagnini
- Stations / Notes
- Positions 1–20 and 41–76 (7 t), 30–35 (12 t), 21–24 (26 t)
Marathon Plus™/Marathon®, 112/114 Style, Vulcan
- Compatible punch presses
- Murata Wiedemann
- Stations / Notes
- Mate is an OEM supplier to Murata Wiedemann
Materials commonly processed: carbon steel, stainless steel and aluminum. If the machine's system isn't known, its make and model are enough to check compatibility, free of charge.
Thick Turret
Tooling systems for thick turret punch presses. Covers the standard turret operations: piercing, blanking, slitting, and nibbling, in mild steel, stainless steel, and aluminum. The standard system reaches, at Mate's recommended thicknesses, up to 3.99 mm mild steel and 2.90 mm stainless; the Heavy Duty variant goes up to 6.35 mm. See also the Thick Turret compatibility guide: A–E stations and the machines covered.

| System | Key differentiator | Catalog |
|---|---|---|
| UltraTEC® | Tool-free punch and stripper changes · 4 mm more regrind life than Original Style · Side stripper change with ball-lock retention (A–B stations) | |
| UltraXT™ | Tool-free stripper change · Regrind life 3.00 mm (A/B stations) and 2.00 mm (C/D/E stations) · Click-to-fit length adjustment (no shims) · Internal and external lubrication · Hardened guides · SLUG FREE® design · Optional M4PM™ | |
| Original Style | The classic Mate Thick Turret reference system | |
| Rapidset™ | Adjustable canisters | – |
| Ultra® IMT Multi Tool | The only fully indexable multi tool: reaches any angle on the part, not just one fixed angle like standard multi tools · 3-station version: UltraTEC® B-station (1¼") punches and tool holders, B-station dies, max. 6 mm material, max. 16 tons (142 kN) · 8-station version: UltraTEC® A-station (½") punches and tool holders, A-station dies, max. 6 mm material, max. 7 tons (62 kN) | |
| MXC™ | Replacement system for Wilson HP, HP WLS, and HP ABS tool holders (100% compatible) · DuraSteel™ steel punches · Also fits UltraTEC® and Ultra XT™ tool holders · Slug Free® dies · A and B stations | |
| AMX™ | Replacement system for Amada ABS assemblies and tool holders (100% compatible) · M2 high-speed-steel punches, OEM-equivalent · Fits UltraTEC® and UltraTEC® Fully Guided tool holders · A–E stations | |
| VersaDie™ | Dies with replaceable inserts | |
| Slug Free® Dies | Dual-taper design, eliminates slug pulling | |
| Mate Pilot™ | Turret calibration: Check and Align modes · One-piece special steel construction |
UltraTEC®
- Key differentiator
- Tool-free punch and stripper changes · 4 mm more regrind life than Original Style · Side stripper change with ball-lock retention (A–B stations)
- Catalog
UltraXT™
- Key differentiator
- Tool-free stripper change · Regrind life 3.00 mm (A/B stations) and 2.00 mm (C/D/E stations) · Click-to-fit length adjustment (no shims) · Internal and external lubrication · Hardened guides · SLUG FREE® design · Optional M4PM™
- Catalog
Original Style
- Key differentiator
- The classic Mate Thick Turret reference system
- Catalog
Rapidset™
- Key differentiator
- Adjustable canisters
Ultra® IMT Multi Tool
- Key differentiator
- The only fully indexable multi tool: reaches any angle on the part, not just one fixed angle like standard multi tools · 3-station version: UltraTEC® B-station (1¼") punches and tool holders, B-station dies, max. 6 mm material, max. 16 tons (142 kN) · 8-station version: UltraTEC® A-station (½") punches and tool holders, A-station dies, max. 6 mm material, max. 7 tons (62 kN)
- Catalog
MXC™
- Key differentiator
- Replacement system for Wilson HP, HP WLS, and HP ABS tool holders (100% compatible) · DuraSteel™ steel punches · Also fits UltraTEC® and Ultra XT™ tool holders · Slug Free® dies · A and B stations
- Catalog
AMX™
- Key differentiator
- Replacement system for Amada ABS assemblies and tool holders (100% compatible) · M2 high-speed-steel punches, OEM-equivalent · Fits UltraTEC® and UltraTEC® Fully Guided tool holders · A–E stations
- Catalog
VersaDie™
- Key differentiator
- Dies with replaceable inserts
- Catalog
Slug Free® Dies
- Key differentiator
- Dual-taper design, eliminates slug pulling
- Catalog
Mate Pilot™
- Key differentiator
- Turret calibration: Check and Align modes · One-piece special steel construction
- Catalog
Trumpf system
Mate tooling compatible with Trumpf punch presses. Mate divides Trumpf and Trumpf-compatible machines into four groups, by alignment-ring and stripper type: Non-Keyed (A), Keyed (E), Rotational (H), and Minimatic (S). The alignment ring differs by group and by size, so your machine's exact model determines the part.

| System | Description | Catalog |
|---|---|---|
| NEXT™ Insert Tooling | Replaceable-insert system, high performance | |
| Trumpf Style Tool Cartridges | OEM-compatible Mate cartridges for TruPunch 200/500R/600L/1000/2000/2010L/2020R/3000/3000L/5000R/6000L · Fiber-reinforced polymer + steel construction · Available as a complete assembly or separately (cartridge / die plate) | |
| Trumpf Standard Size 1 | Directly compatible with Trumpf machines | |
| Trumpf Standard Size 2 | Directly compatible with Trumpf machines | |
| LongLife™ Slitting | Long-life slitting tools | |
| Tool Cassettes | Trumpf tool cassettes | – |
| M4PM™ Steel Tooling | M4PM steel tooling for special applications |
NEXT™ Insert Tooling
- Description
- Replaceable-insert system, high performance
- Catalog
Trumpf Style Tool Cartridges
- Description
- OEM-compatible Mate cartridges for TruPunch 200/500R/600L/1000/2000/2010L/2020R/3000/3000L/5000R/6000L · Fiber-reinforced polymer + steel construction · Available as a complete assembly or separately (cartridge / die plate)
- Catalog
Trumpf Standard Size 1
- Description
- Directly compatible with Trumpf machines
- Catalog
Trumpf Standard Size 2
- Description
- Directly compatible with Trumpf machines
- Catalog
LongLife™ Slitting
- Description
- Long-life slitting tools
- Catalog
Tool Cassettes
- Description
- Trumpf tool cassettes
M4PM™ Steel Tooling
- Description
- M4PM steel tooling for special applications
- Catalog
Multi Tool PDS
A multi tool system turns a single turret indexing station into a holder for multiple punch-and-die sets, positioned one at a time on each hit. A 20-station turret can reach 22-27 active tools this way, without an extra machine. The benefits Mate states are greater nesting freedom, shorter setup time, and more tooling capacity on the same machine.

Thick Turret forming tools
Ultraform and Roller Solutions systems for forming operations. Typical operations are stiffening ribs, cross-brakes, offsets, embossing, countersinks for screw heads, thread extrusions, and deburring, all done directly on the punch press, without a separate pass at the press brake. Mate gives HVAC ductwork as a concrete example, where parts have many ribs and cross-brakes, and window/enclosure manufacturers, where an offset form around cutouts adds rigidity and gives a mounting point for a gasket or trim. A stiffening rib increases part rigidity, which sometimes allows a switch to thinner material than the design originally called for.

| System | Description | Catalog |
|---|---|---|
| Ultraform® Insert | Forming tool holder system with inserts | |
| Ultraform XT™ | XT forming tool holders | |
| Ultraform FX™ | Forming with stroke control | |
| Ultraform PF | PF forming tool holders, details in the catalog | |
| Rolling Pincher™ | Cuts at any angle with auto-indexing · Virtually no burrs or nibble marks · No scrap · Slit can start or end anywhere on the sheet · Steel 0.80–2.00 mm · Stainless 0.80–1.50 mm · Aluminum 0.80–2.49 mm · Min. radius 500 mm | |
| Rolling Rib™ | Ribs along any contour with auto-indexing · No cutting through · Steel 0.80–2.00 mm · Stainless 0.80–1.50 mm · Aluminum 0.80–2.49 mm | |
| Rolling Shear™ | Cuts along any contour with auto-indexing · No burrs or witness marks · No scrap · Steel 0.80–2.00 mm · Stainless 0.80–1.50 mm · Aluminum 0.80–2.49 mm · Min. radius 45–100 mm | |
| Rolling Offset™ | Offsets along any contour · Stock sizes 1.50–3.00 mm · Steel 0.80–2.00 mm · Stainless 0.80–1.50 mm · Aluminum 0.80–2.49 mm · Min. radius 25 mm |
Ultraform® Insert
- Description
- Forming tool holder system with inserts
- Catalog
Ultraform XT™
- Description
- XT forming tool holders
- Catalog
Ultraform FX™
- Description
- Forming with stroke control
- Catalog
Ultraform PF
- Description
- PF forming tool holders, details in the catalog
- Catalog
Rolling Pincher™
- Description
- Cuts at any angle with auto-indexing · Virtually no burrs or nibble marks · No scrap · Slit can start or end anywhere on the sheet · Steel 0.80–2.00 mm · Stainless 0.80–1.50 mm · Aluminum 0.80–2.49 mm · Min. radius 500 mm
- Catalog
Rolling Rib™
- Description
- Ribs along any contour with auto-indexing · No cutting through · Steel 0.80–2.00 mm · Stainless 0.80–1.50 mm · Aluminum 0.80–2.49 mm
- Catalog
Rolling Shear™
- Description
- Cuts along any contour with auto-indexing · No burrs or witness marks · No scrap · Steel 0.80–2.00 mm · Stainless 0.80–1.50 mm · Aluminum 0.80–2.49 mm · Min. radius 45–100 mm
- Catalog
Rolling Offset™
- Description
- Offsets along any contour · Stock sizes 1.50–3.00 mm · Steel 0.80–2.00 mm · Stainless 0.80–1.50 mm · Aluminum 0.80–2.49 mm · Min. radius 25 mm
- Catalog
Special applications
Tooling for specific applications frequently encountered in sheet metal working. The common thread across this family is that it eliminates a secondary operation (a pass at the press brake, manual deburring after separating parts from a nest, a separate marking setup), doing it directly on the punch press instead.
| Product | Application | Catalog |
|---|---|---|
| EasyBend™ | Scores a bend line on the punched part for later hand bending, eliminates a separate press-brake operation for small parts or short runs. Not a replacement for a press brake in volume production | |
| EasyMark™ | Sheet marking | |
| EasySnap™ | Controlled snap-off | |
| EasyTap™ | Sheet metal tapping | – |
| HexLock™ | Form-and-lance assembly with triple reverse spring · Retains DIN933 screws and DIN934 nuts in sheet metal (M5, M6, M8) · Prevents rotation through mechanical grip · Works with metric or imperial fasteners | |
| Rollerball™ | Creates beads, stiffening ribs, or offset forms directly on the punch press, without a separate press-brake operation · Can replace hundreds of hits with a single pass for a continuous rib | |
| Rollerball Deburr™ | Deburring | |
| Sheetmarker™ | Marking or etching on sheet metal without surface damage · Brass insert available for local removal of protective film on aluminum or stainless steel, ahead of welding or laser cutting |
EasyBend™
- Application
- Scores a bend line on the punched part for later hand bending, eliminates a separate press-brake operation for small parts or short runs. Not a replacement for a press brake in volume production
- Catalog
EasyMark™
- Application
- Sheet marking
- Catalog
EasySnap™
- Application
- Controlled snap-off
- Catalog
EasyTap™
- Application
- Sheet metal tapping
HexLock™
- Application
- Form-and-lance assembly with triple reverse spring · Retains DIN933 screws and DIN934 nuts in sheet metal (M5, M6, M8) · Prevents rotation through mechanical grip · Works with metric or imperial fasteners
- Catalog
Rollerball™
- Application
- Creates beads, stiffening ribs, or offset forms directly on the punch press, without a separate press-brake operation · Can replace hundreds of hits with a single pass for a continuous rib
- Catalog
Rollerball Deburr™
- Application
- Deburring
- Catalog
Sheetmarker™
- Application
- Marking or etching on sheet metal without surface damage · Brass insert available for local removal of protective film on aluminum or stainless steel, ahead of welding or laser cutting
- Catalog
What to send us so we can identify the right tool
- 1 Your punch press's exact make and model.
- 2 The tooling system or tool holder configuration, if you already know it.
- 3 The station and tool size you need, for Thick Turret requests.
- 4 The operation you need: hole, special shape, marking, bending, plus the material and thickness.
- 5 For special applications or custom tooling: a drawing, a reference part, or photographs.
Not every detail is needed in your first message. We'll check together what's still missing, based on your request.
Frequently asked questions
Do you also run a press brake? UKB press brake tools → shipped from manufacturer stock in 5 to 7 business days.
The tooling system follows from the machine model
Mate publishes compatibility by machine group; the exact punch press model determines the group and the matching tooling.
We'll get back to you once we understand your request.